Machining capabilities
| Process | Machine | Used for |
|---|---|---|
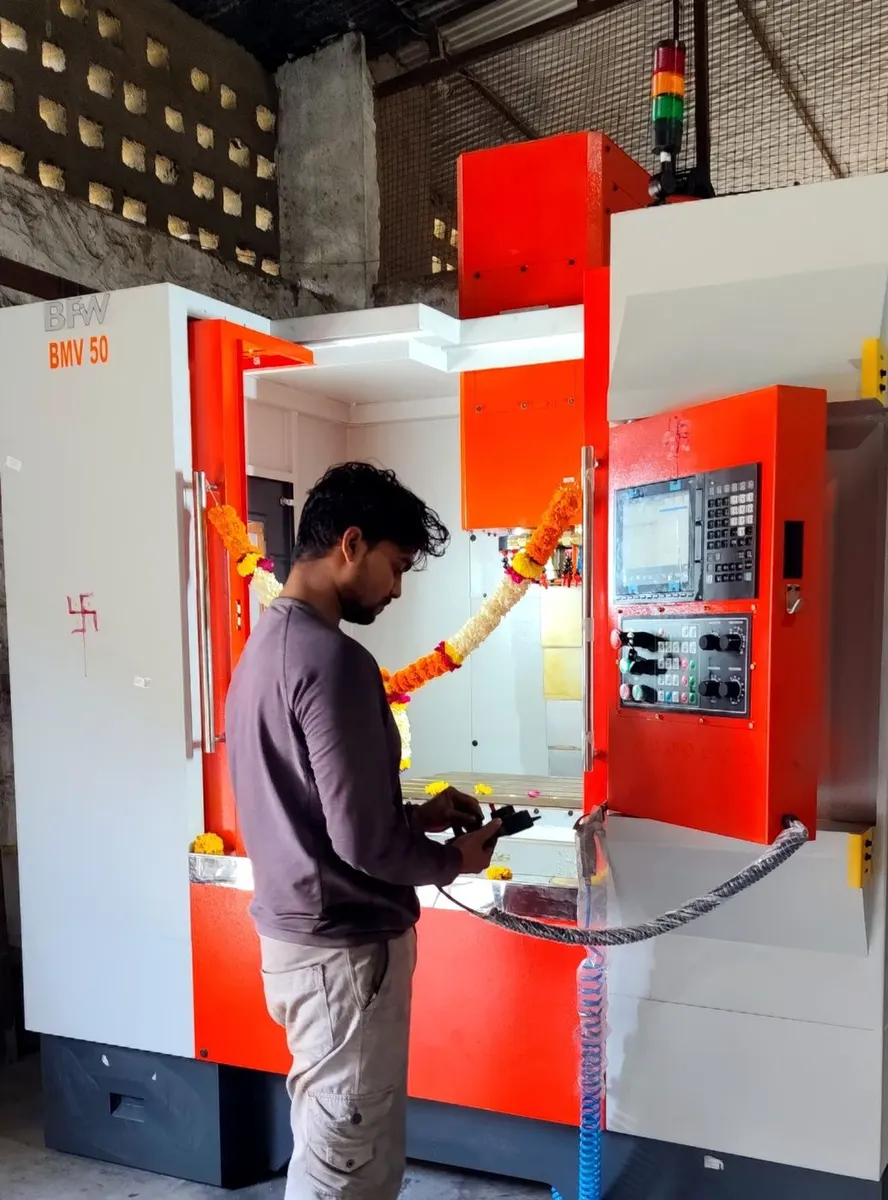
| VMC machining | BFW BMV 50 | Cores, cavities, inserts and plates |
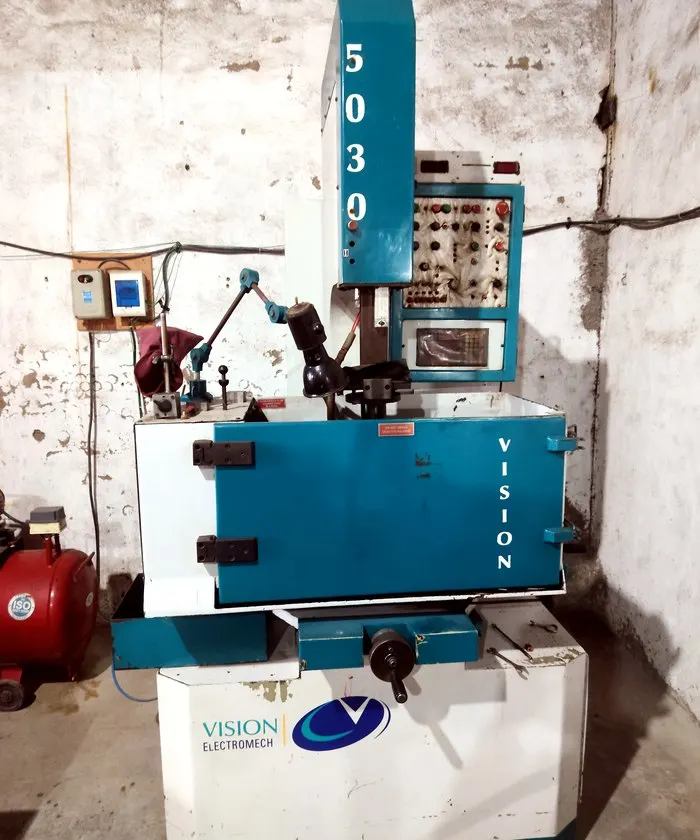
| EDM | Vision Electro | Ribs, engraving, logos, sharp corners |
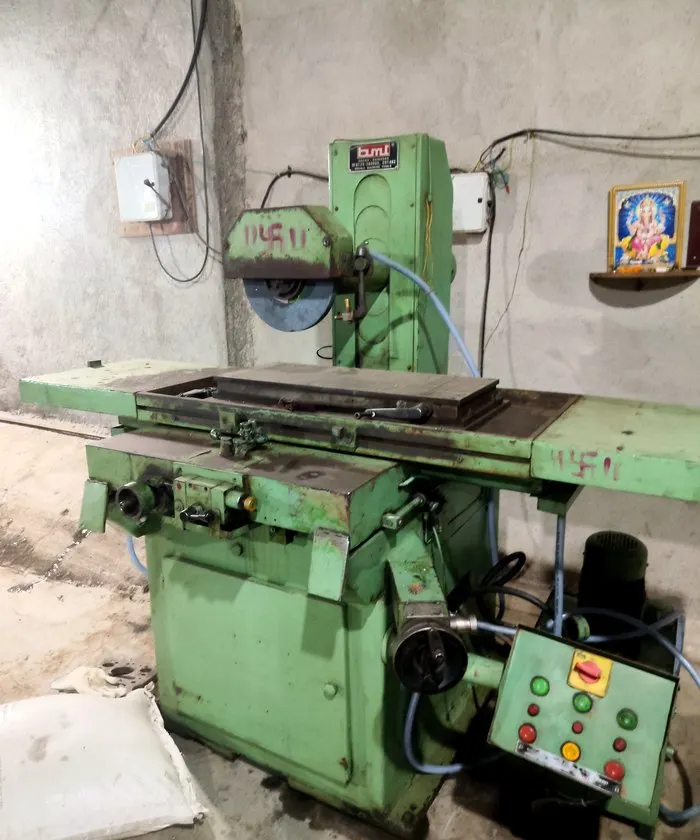
| Surface grinding | HMT surface grinder | Plates and inserts flat and square |
| Turning | 2 lathes | Guide pillars, bushes, pins |
| Fitting and assembly | Bench fitting, blue matching | Shear edges, parting faces, assembly |
Assembly and bench work
Every mould is fitted and assembled by hand in our bench and assembly area. Plates, guide pillars, bushes and ejector parts are laid out, checked and fitted; mould halves are matched at the fitting stand; and chain hoists move heavy plates safely through assembly.
Steels
| Steel | Where we use it |
|---|---|
| H13 (hardened) | Cores, cavities and inserts; die casting inserts |
| Böhler W302 ESR | Cavities for long runs and abrasive compounds; die casting inserts |
| P20 (pre-hardened) | Plates, holders and low-volume tools |
What we build and work on
- Compression moulds for SMC, DMC, BMC, Bakelite, melamine and UF
- Single and multi-cavity moulds
- Flash, positive and semi-positive mould types
- Mould repair, re-polishing and modification
- Die casting die repair, modification and new inserts (HPDC, GDC, LPDC)
EDM: ribs, sharp corners and fine detail
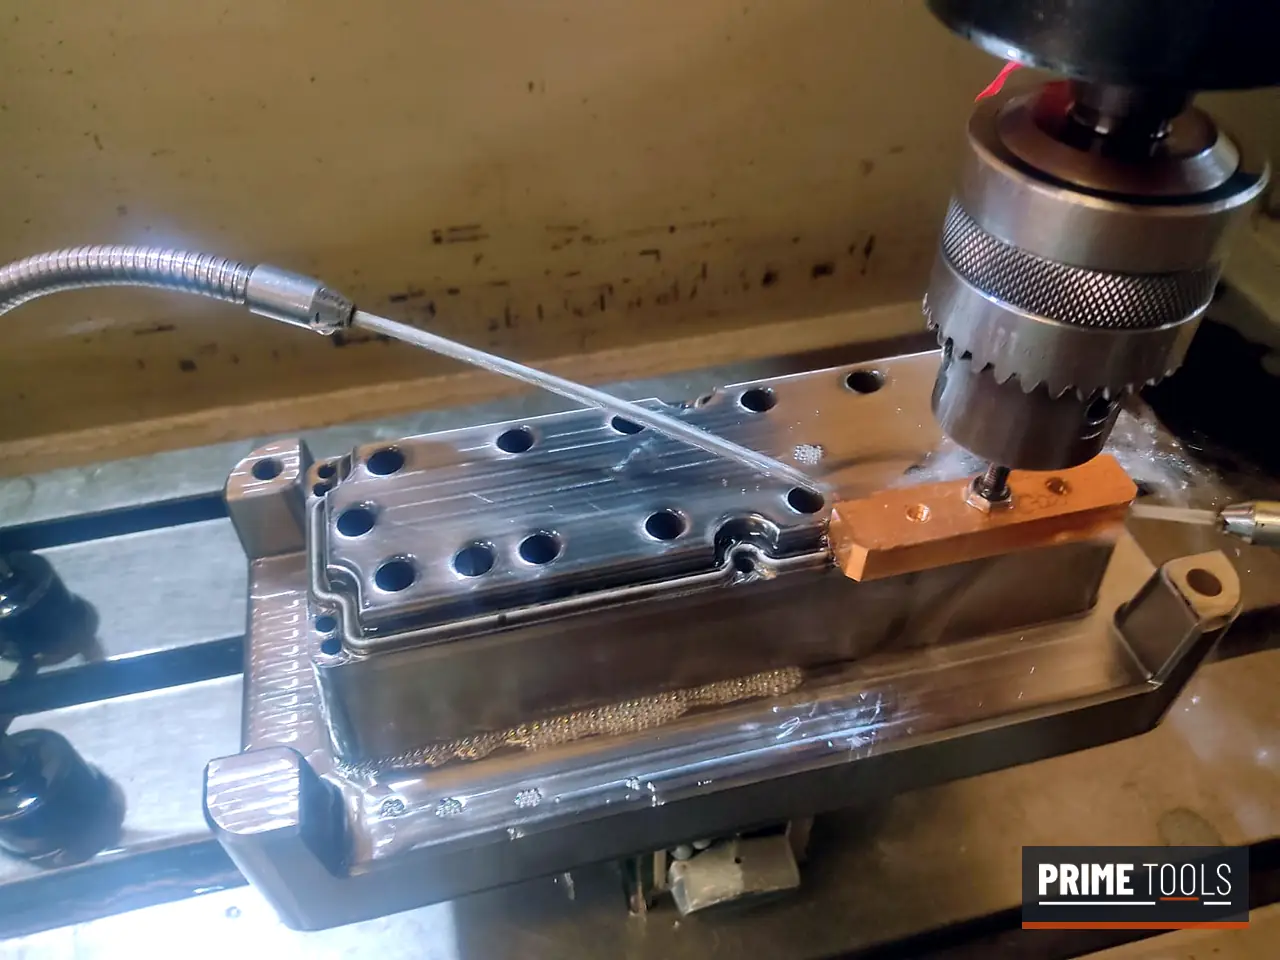
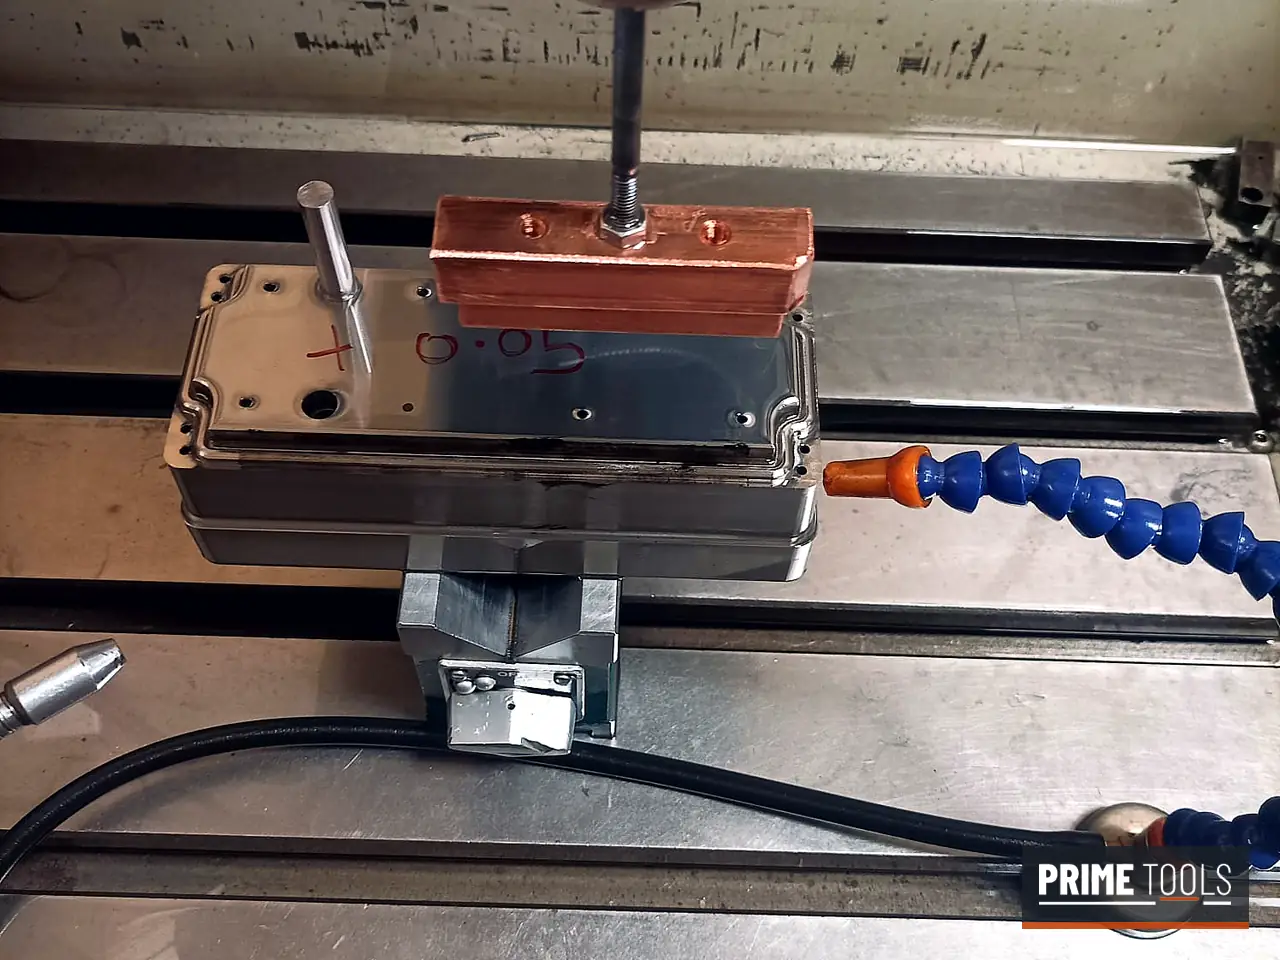
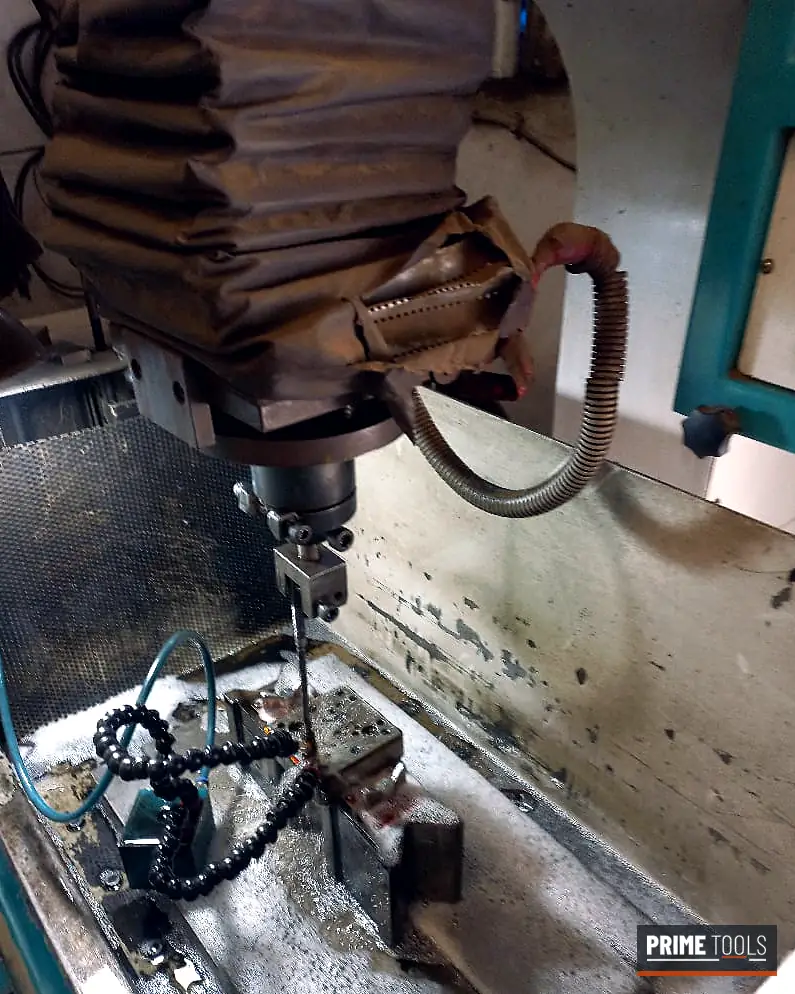
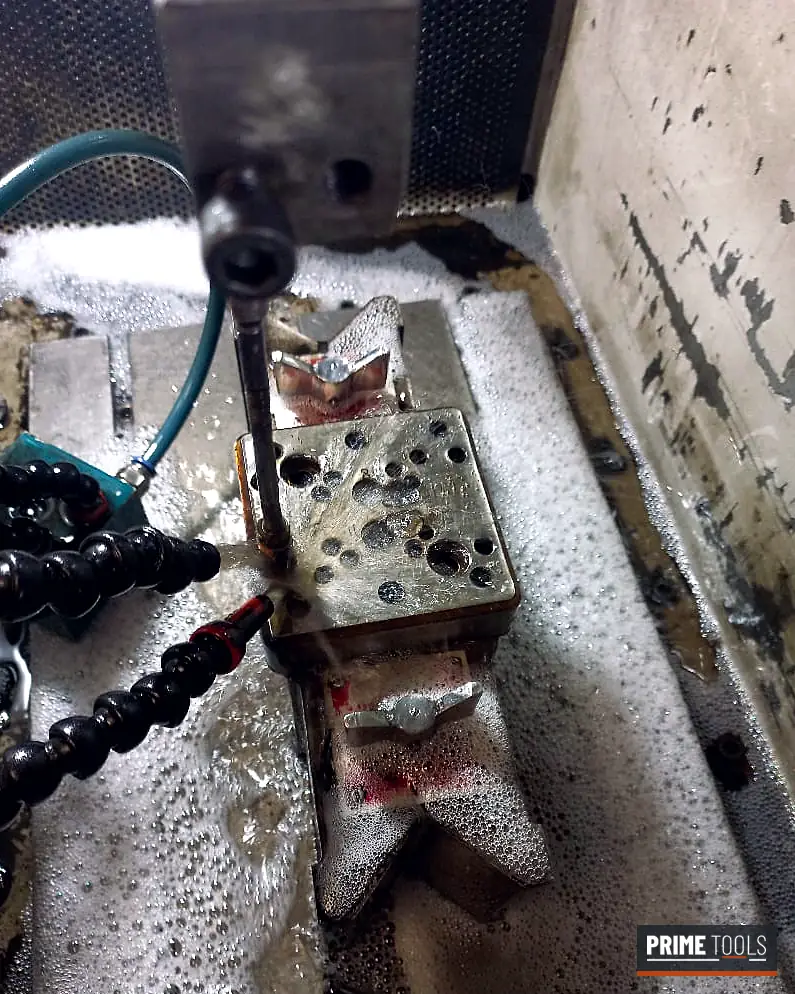
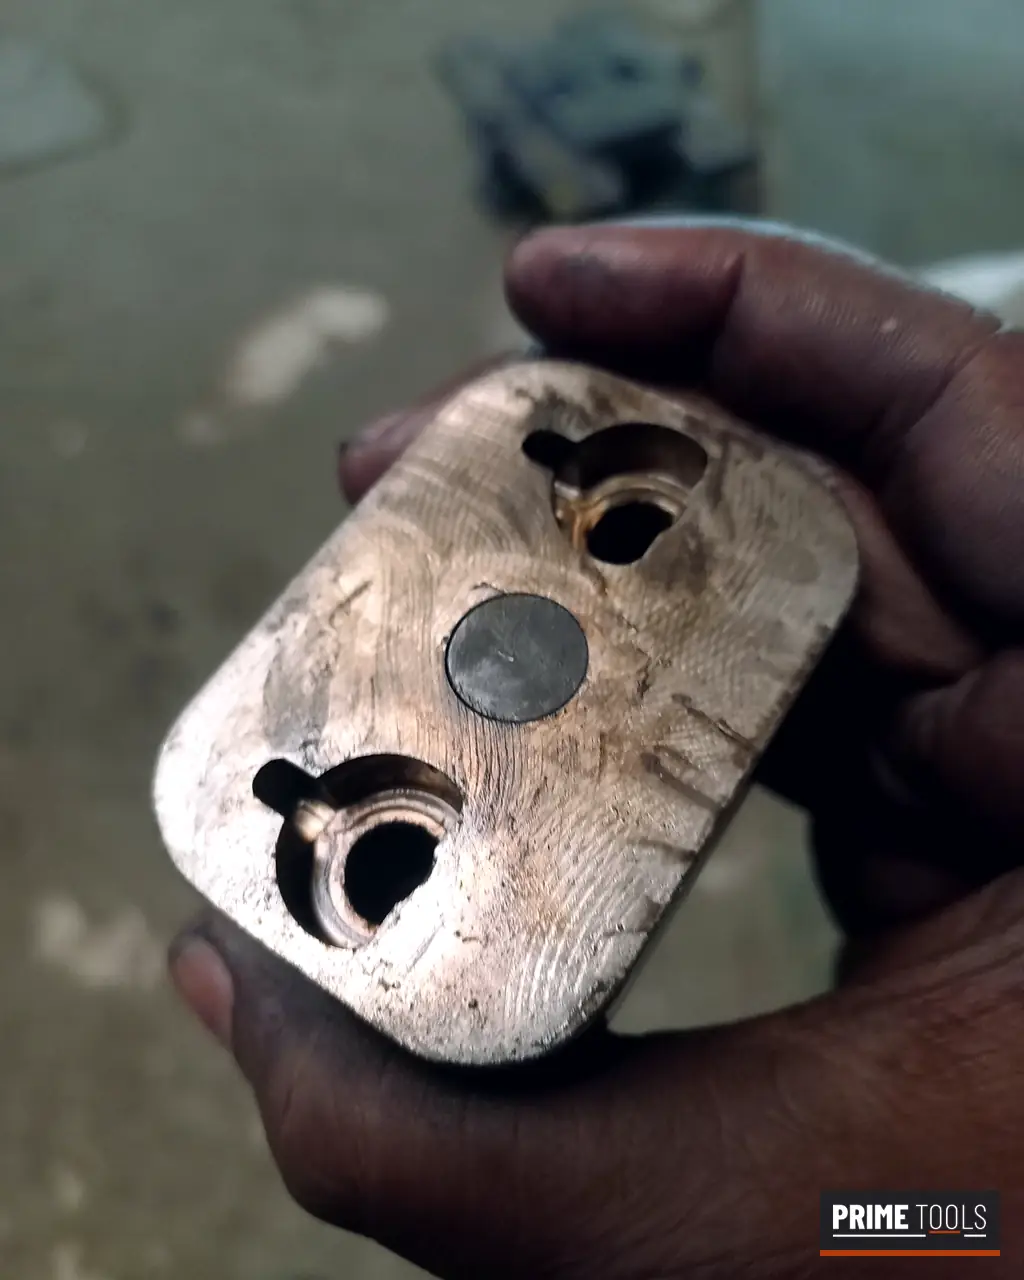
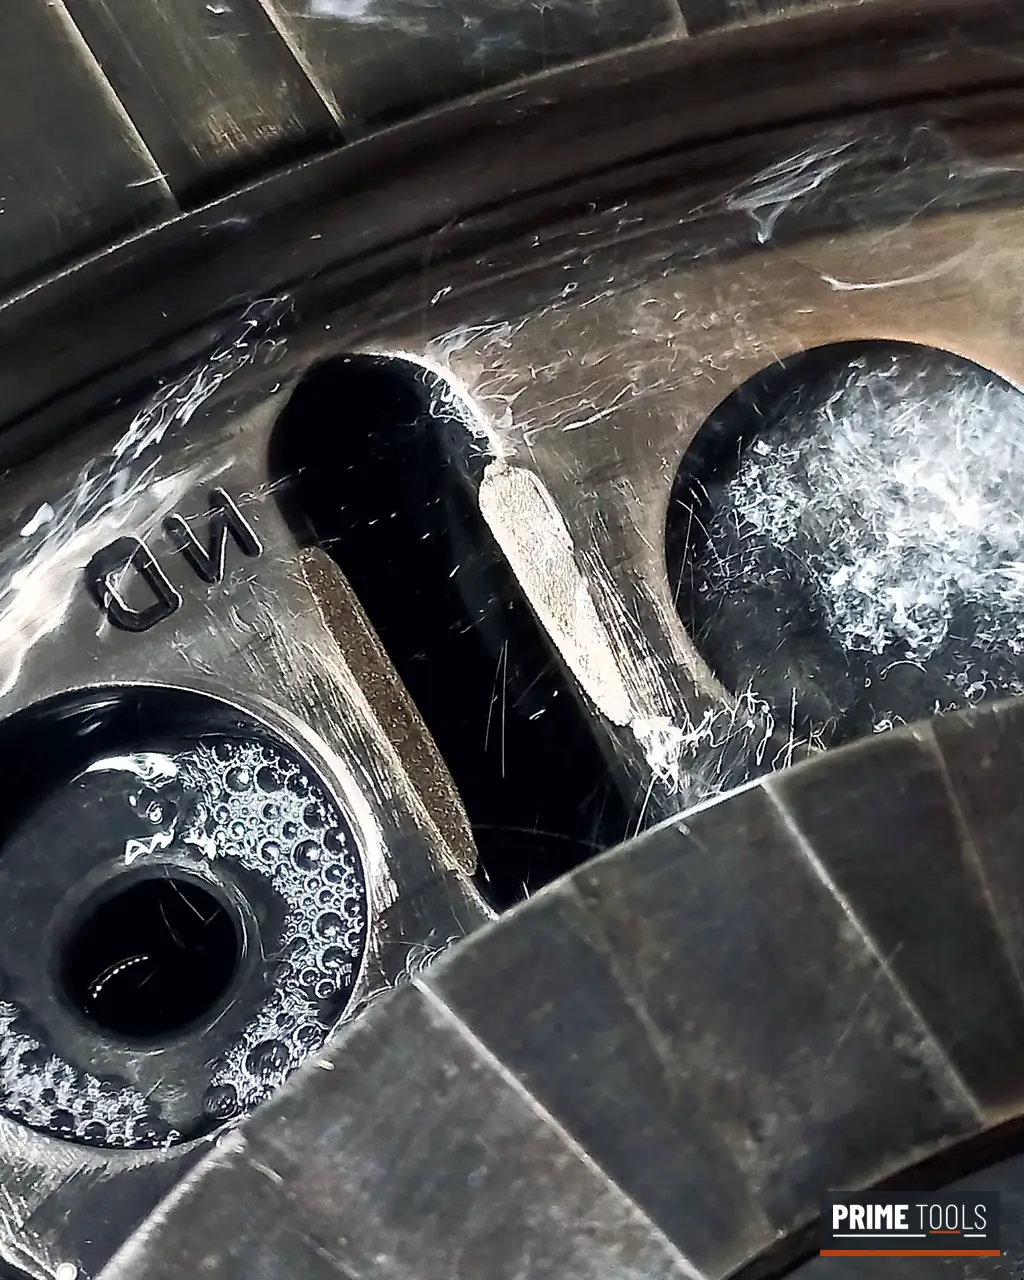
A milling cutter is round, so it cannot cut a sharp inside corner, a deep narrow rib or fine lettering. For these we use EDM (spark erosion): a copper electrode shaped like the feature is sunk into the hardened steel, so the detail is cut after heat treatment without distortion.
We machine the copper electrodes on our VMC, set them square on the EDM, and use roughing and finishing electrodes so the surface comes out ready for polishing. Typical EDM work on our moulds includes rib slots, corner relief, engraving and logos, and repairs inside hardened inserts.
Send your part for a free DFM review
3D model or drawing, material and annual volume. We reply within one working day.