Quality at every stage
- DFM sign-off. The part design and mould concept are agreed before steel is ordered.
- In-process checks. Critical sizes on cores, cavities and inserts are checked during machining.
- Fitting and blue matching. Shear edges and parting faces are blue matched so the mould closes evenly.
- Heating check. Heaters and thermocouples are tested and the surface temperature checked.
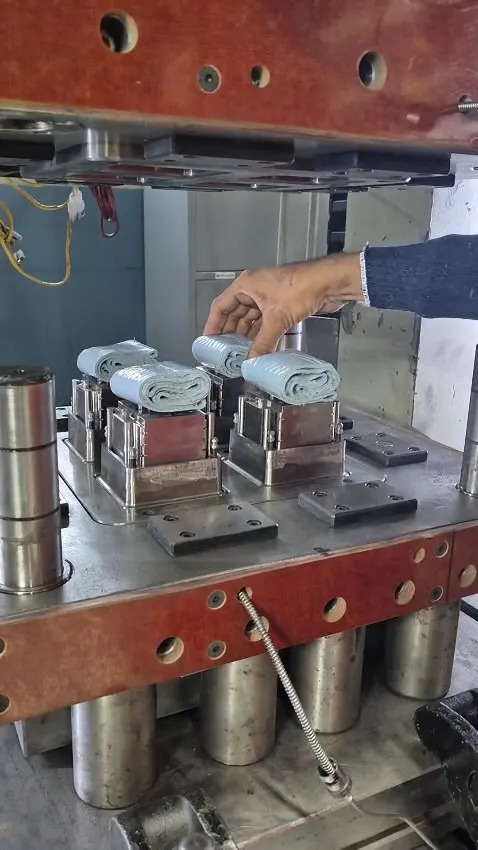
- Press trial. The mould runs on the press with your material, and settings are recorded.
- First-off approval. First-off parts go to you for approval before handover.
What we check at the trial
The trial is where a mould proves itself. We run it on the press with the material grade you will use in production, and we look at the parts as closely as a buyer would. Does the cavity fill completely, including the deep ribs and bosses? Is the flash at the shear edge thin and even all the way round? Does the part release cleanly, without sticking or ejector marks on the visible faces? Is the surface free of blisters, burns and porosity, and does the part sit flat without warpage?
If a part shows a problem, we correct it in the mould before handover, not after. Typical corrections are a shear edge adjustment, extra venting, a change to the charge position or a heating correction. The settings that gave good parts are recorded, so your production team can start from the same point on your press.
For buyers who cannot visit, we share trial photos and video, and send first-off parts by courier. A mould leaves our tool room only after you have approved those parts.
What you receive
- DFM report for the part
- Mould drawings
- Trial record with key settings
- First-off parts for approval
- Maintenance notes for your team
Send your part for a free DFM review
3D model or drawing, material and annual volume. We reply within one working day.