Every project here was designed, machined, fitted and checked by our own team. Most compression mould jobs start with a free DFM review; most repair jobs start with a strip-down and a written list of what we found.
New compression mould: GRP enclosure lid
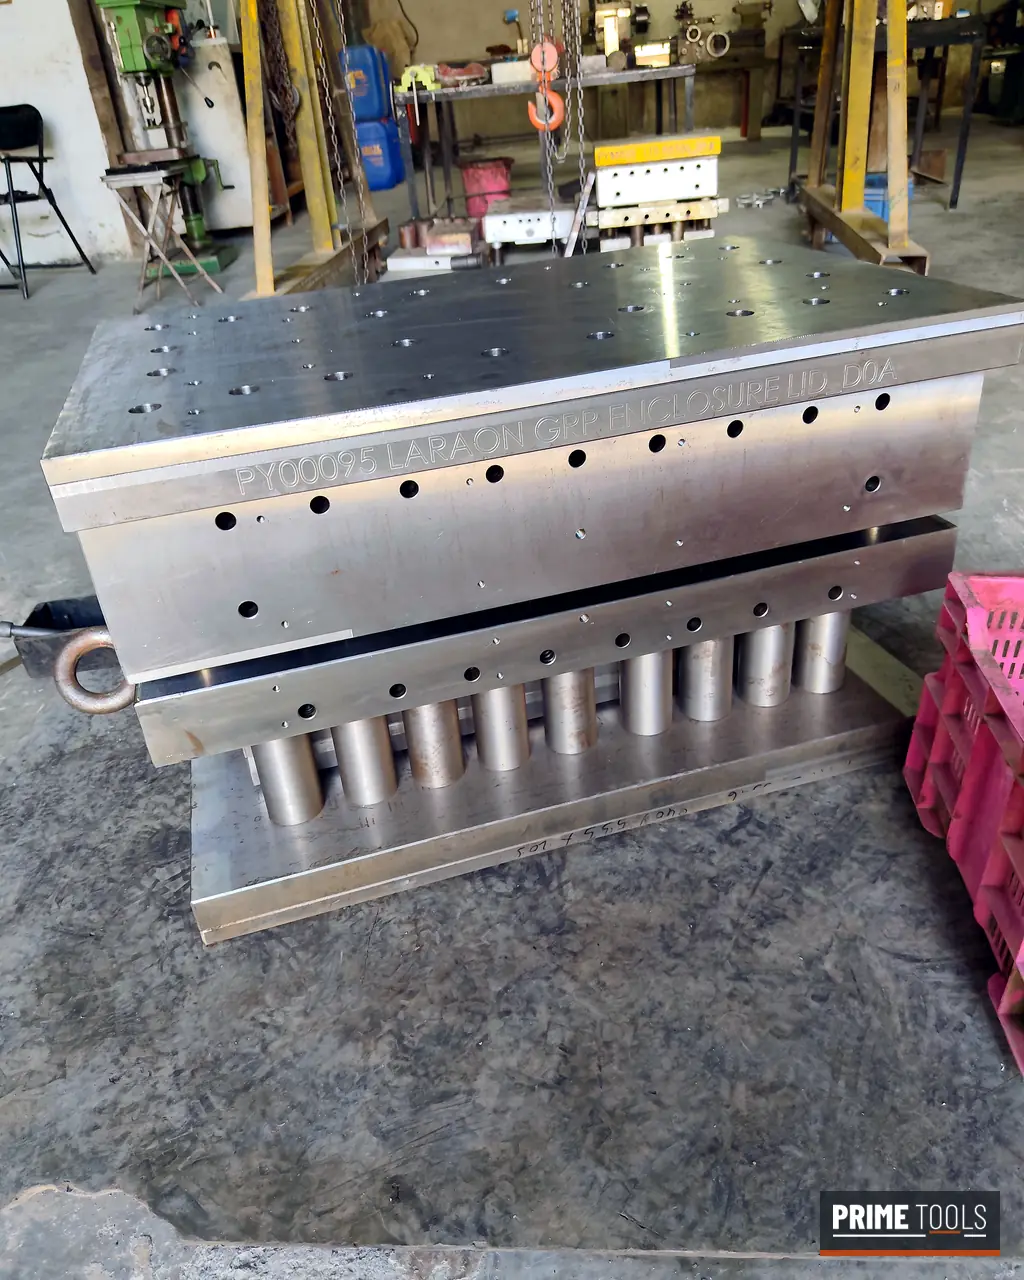
A new compression mould for the lid of an outdoor GRP (SMC) electrical enclosure. The lid needs a flat sealing face for the gasket, stiff ribs on the inside and clean edges on the outside, because it is the face of the product.
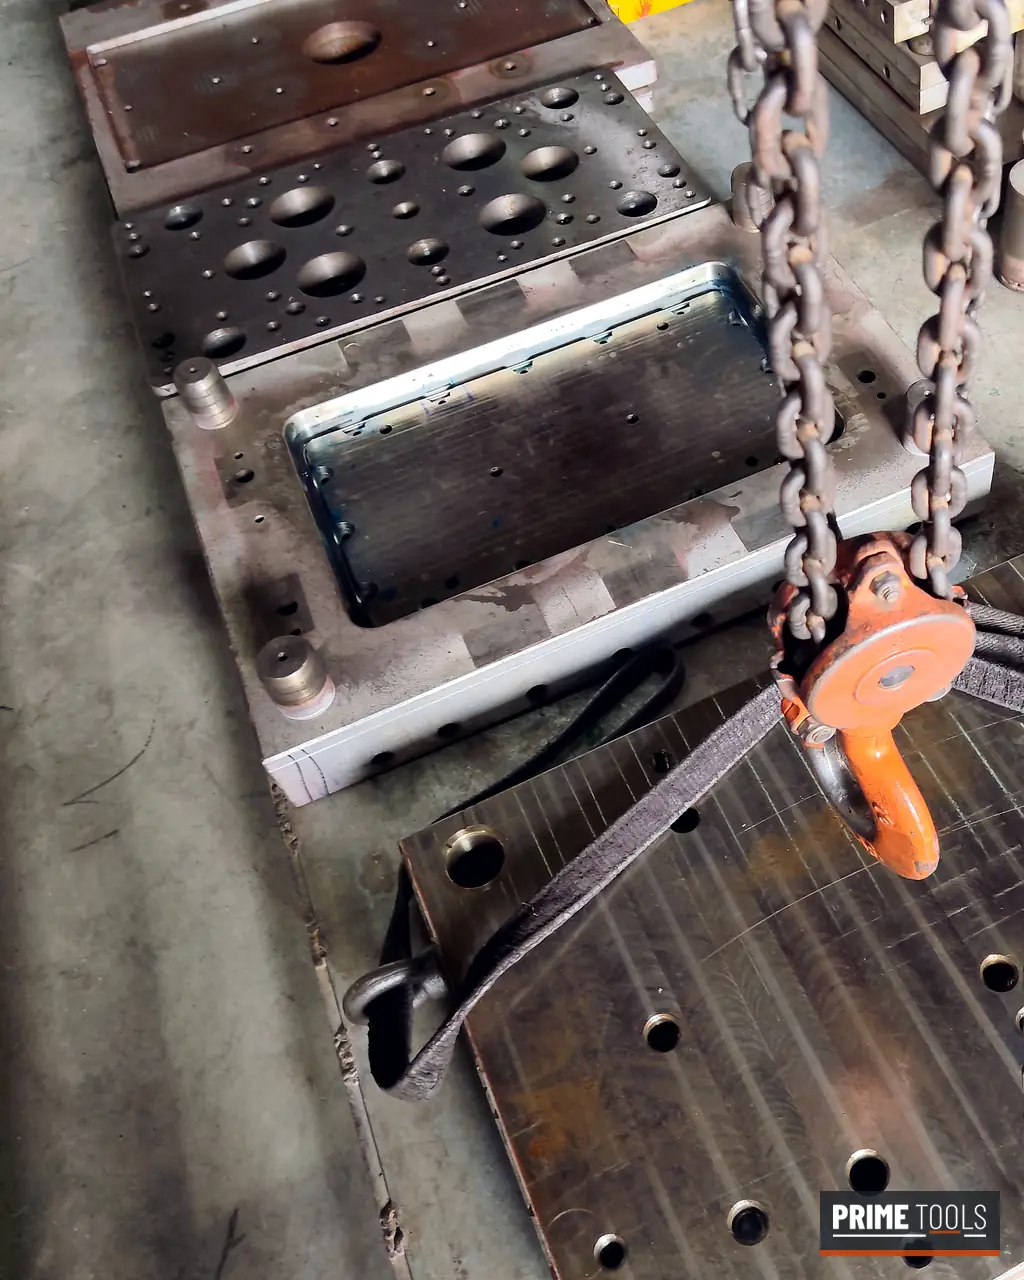
We built the core and cavity halves on our VMC, fitted the guide pillars and bushes, set the ejector system and blue matched the shear edge so the mould closes evenly and flash stays thin. The mould was assembled, heated and checked before trial.
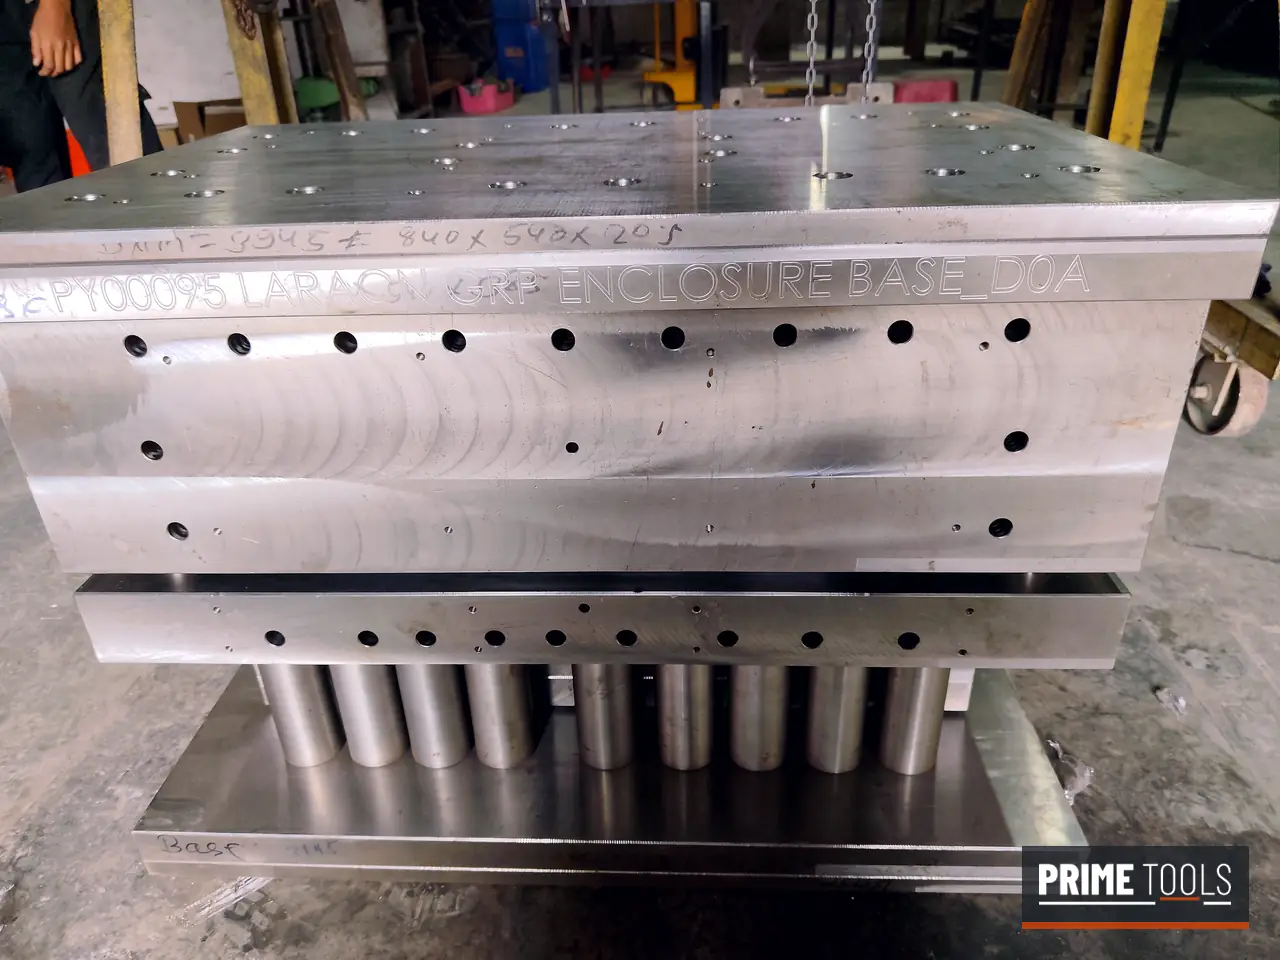
New compression mould: GRP enclosure base
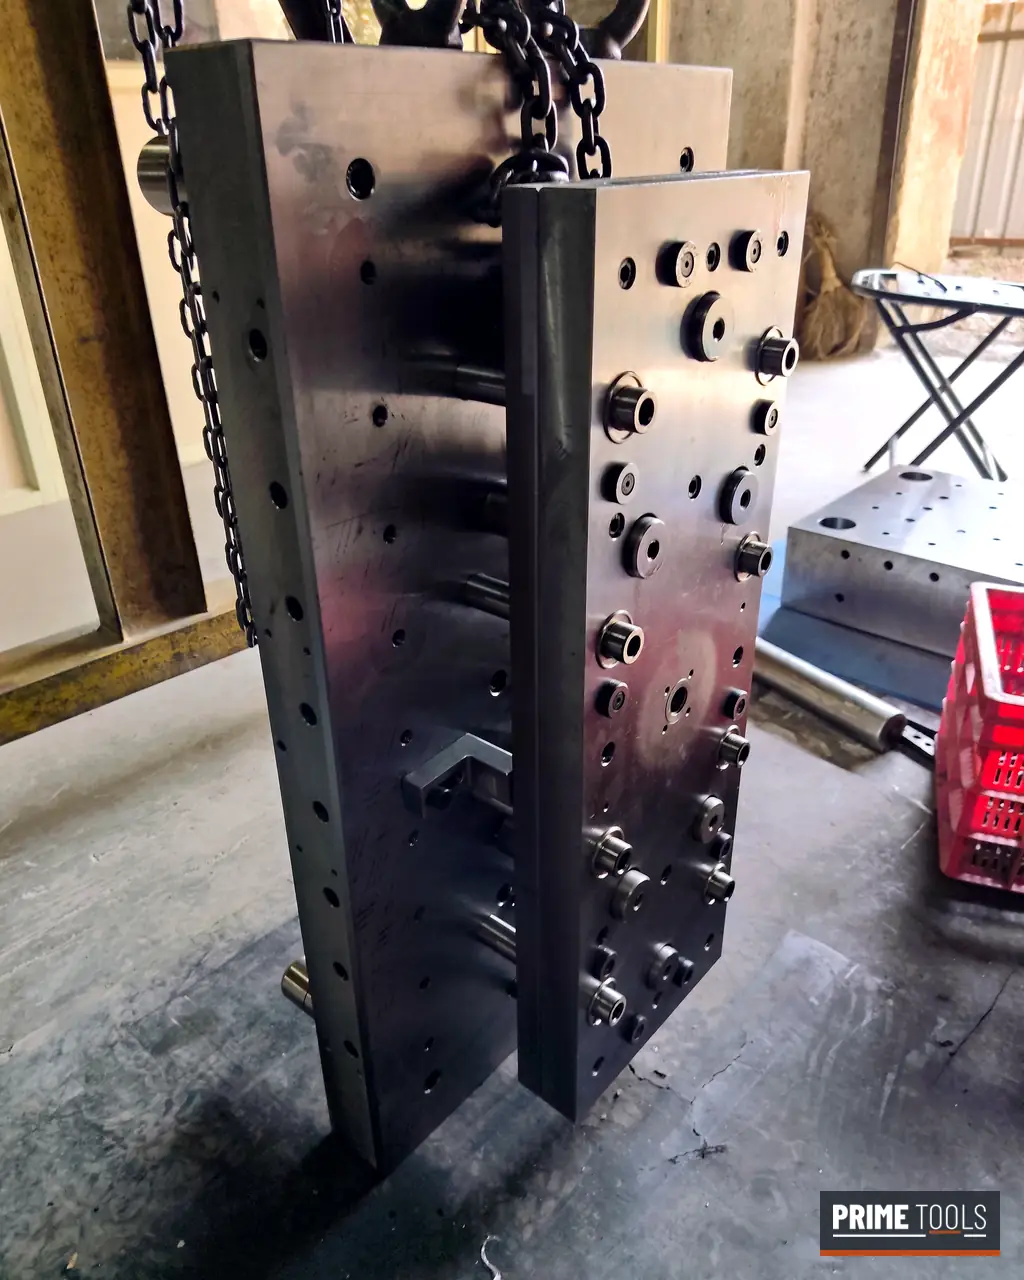
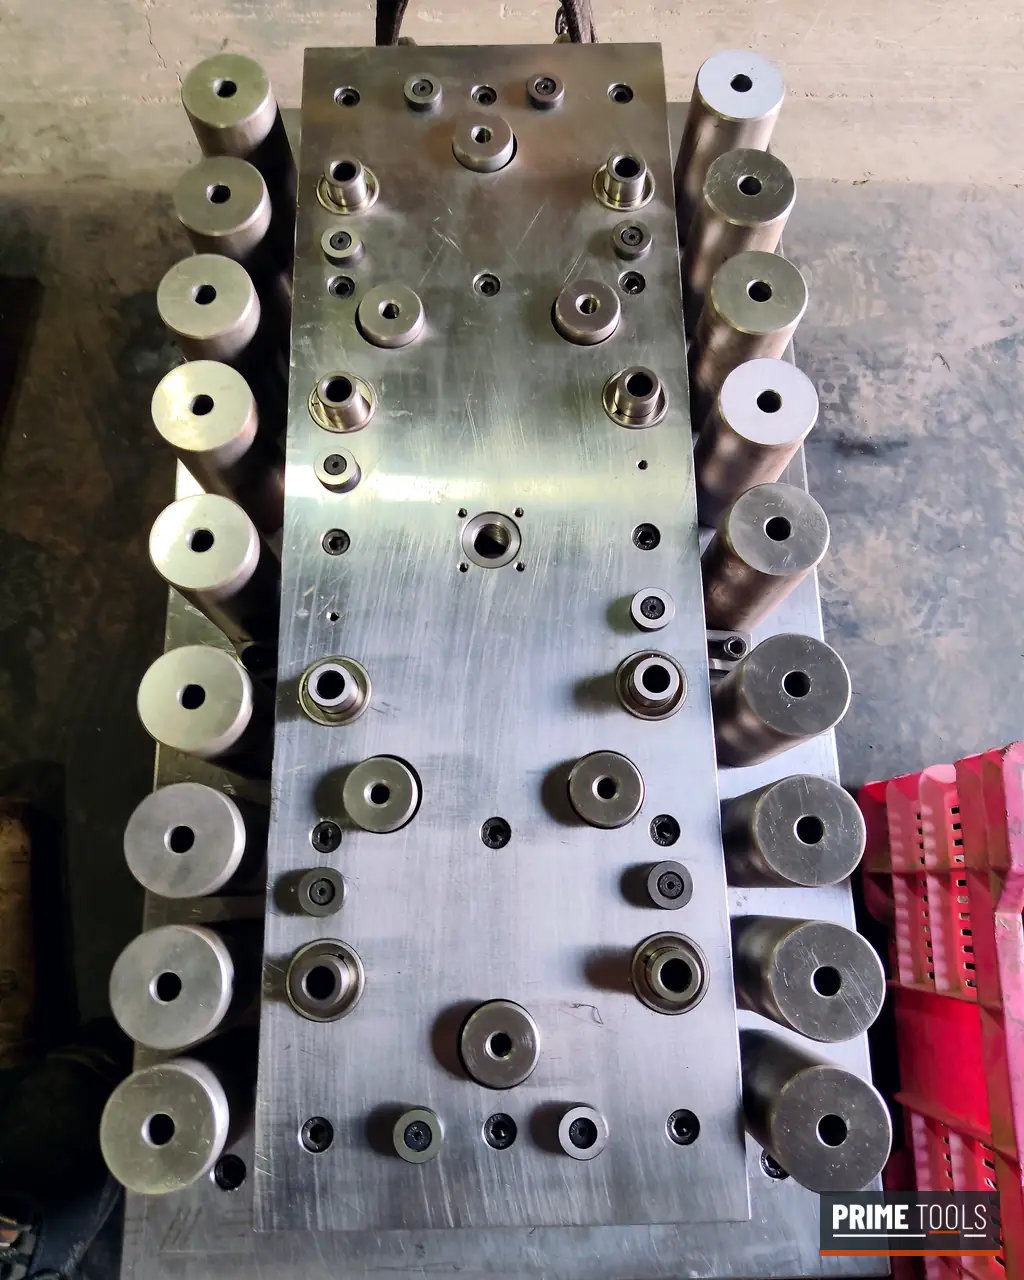
The matching base mould for the same enclosure family. A deep box with draft on every wall, an even wall section and bosses for mounting, so the SMC charge flows to the corners and the part releases cleanly.
Base and lid were designed together so the two parts meet on one sealing line. Both were reviewed in DFM before steel was cut, then machined, fitted and trialled in our tool room.
New compression mould: gasket holder frame
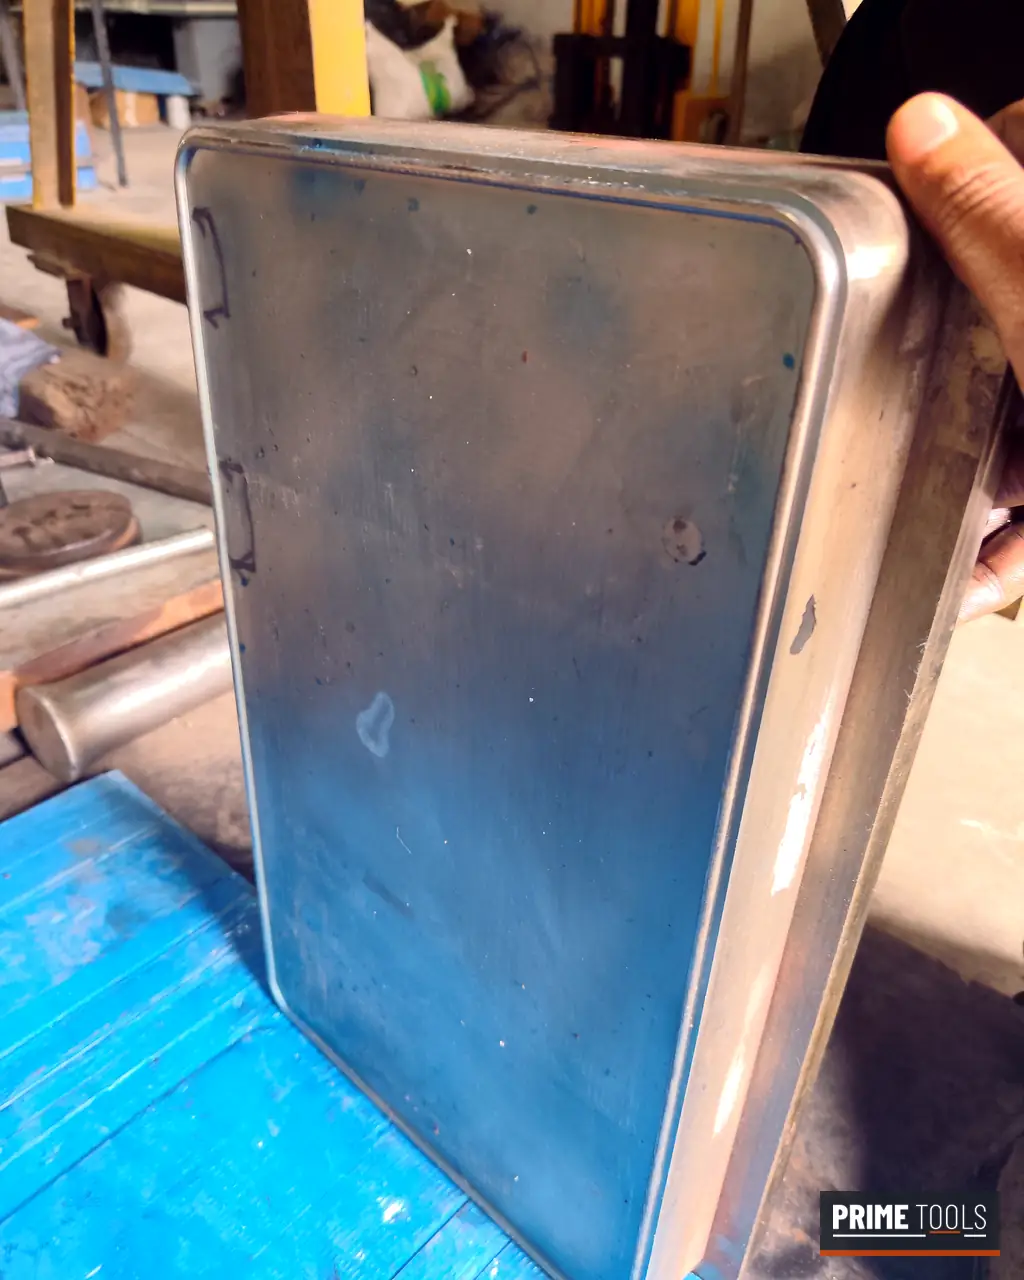
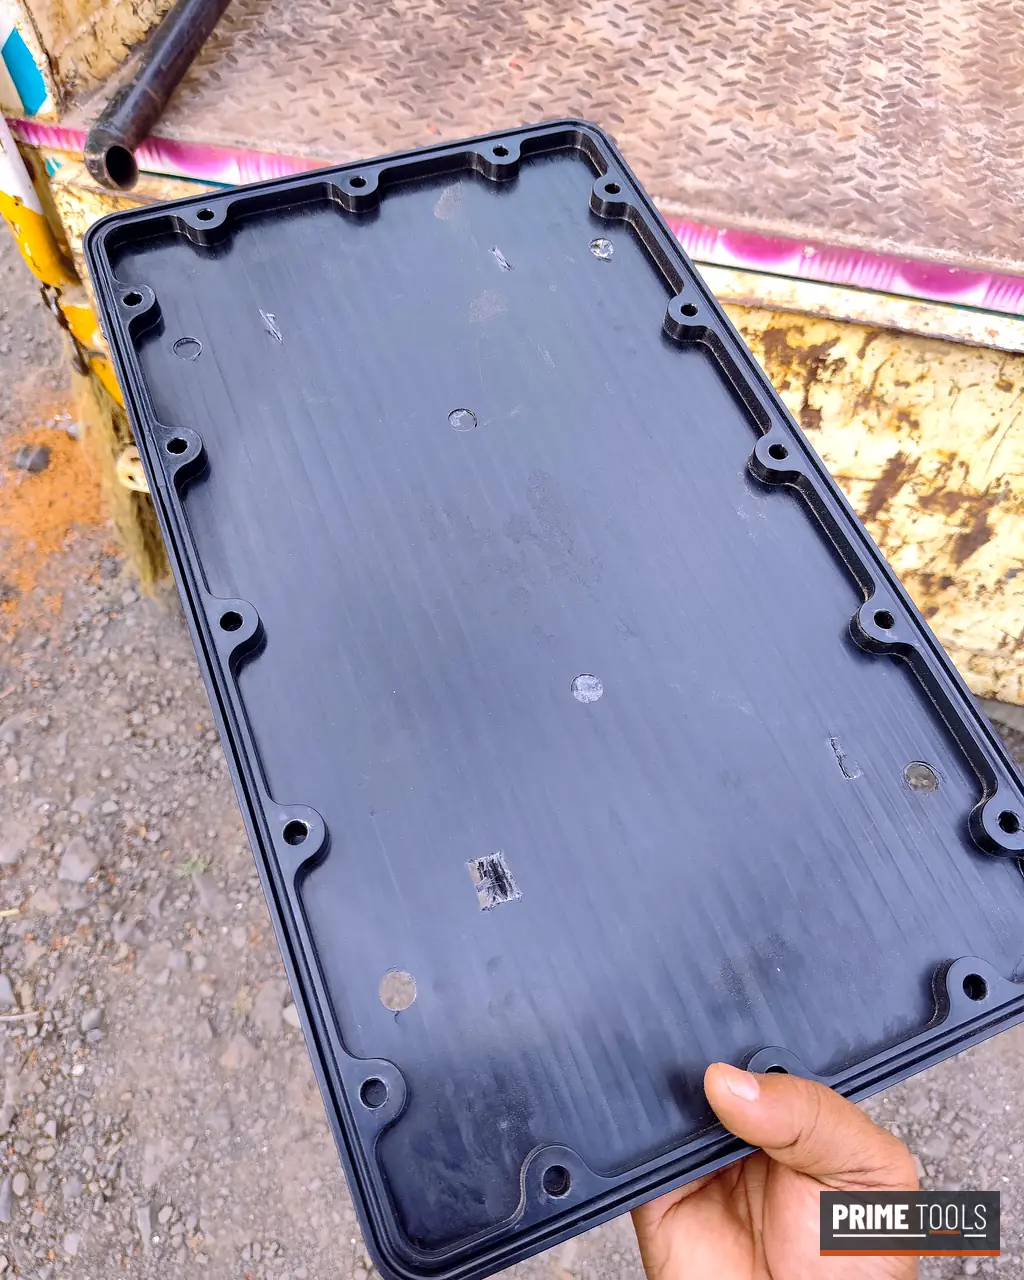
A thin, flat frame that holds the gasket of an enclosure door. Thin and wide parts like this warp easily, so the mould needs even heating across the whole plate and a polished cavity so the part releases without bending.
The cavity was machined, polished and fitted, and the first parts came off flat with clean holes and edges.
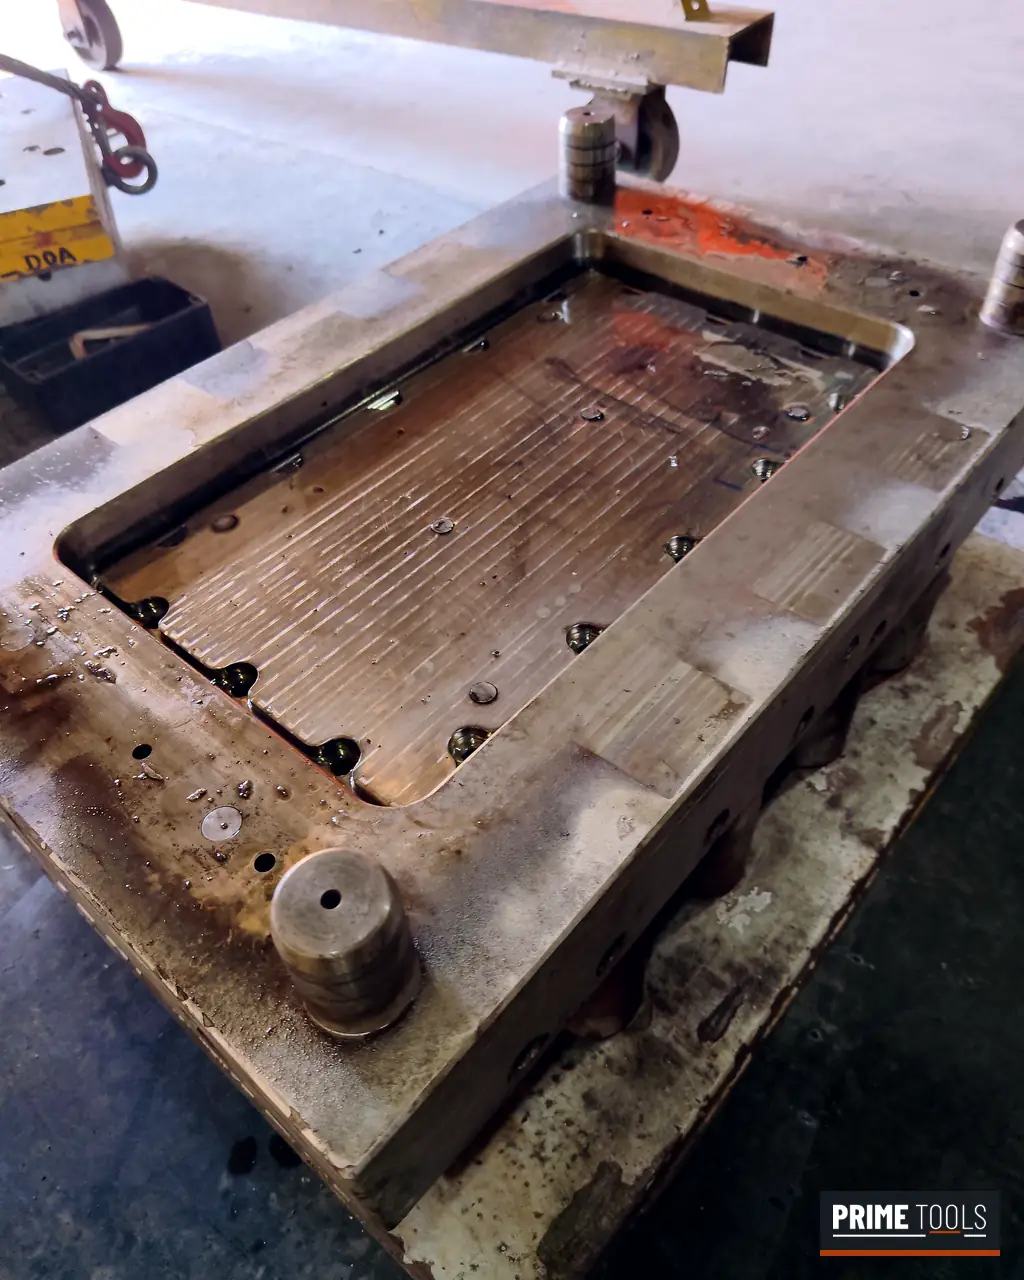
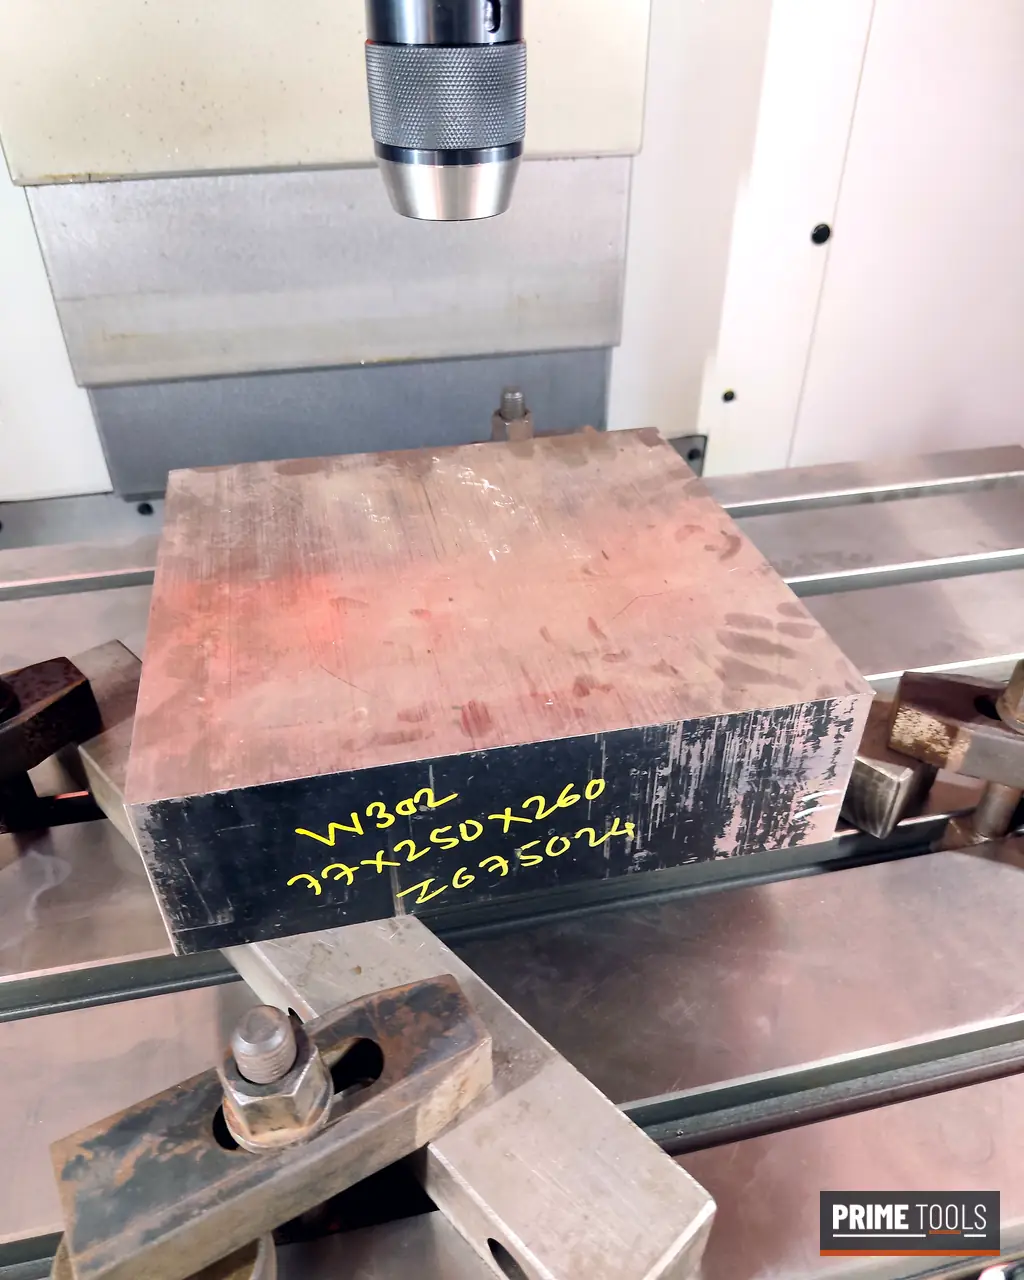
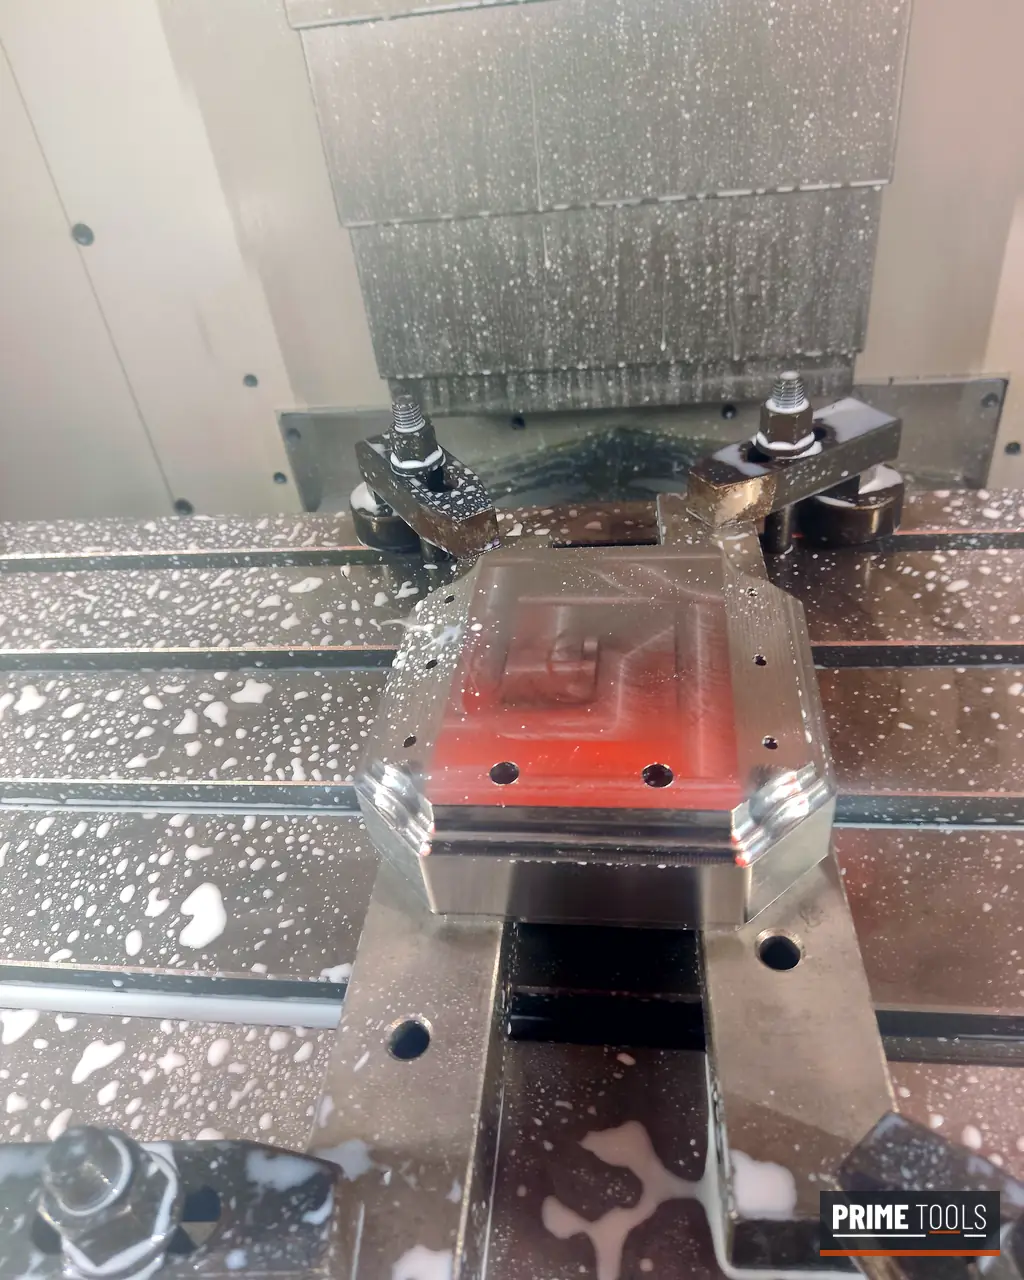
Lid cavity machined from a solid W302 ESR block
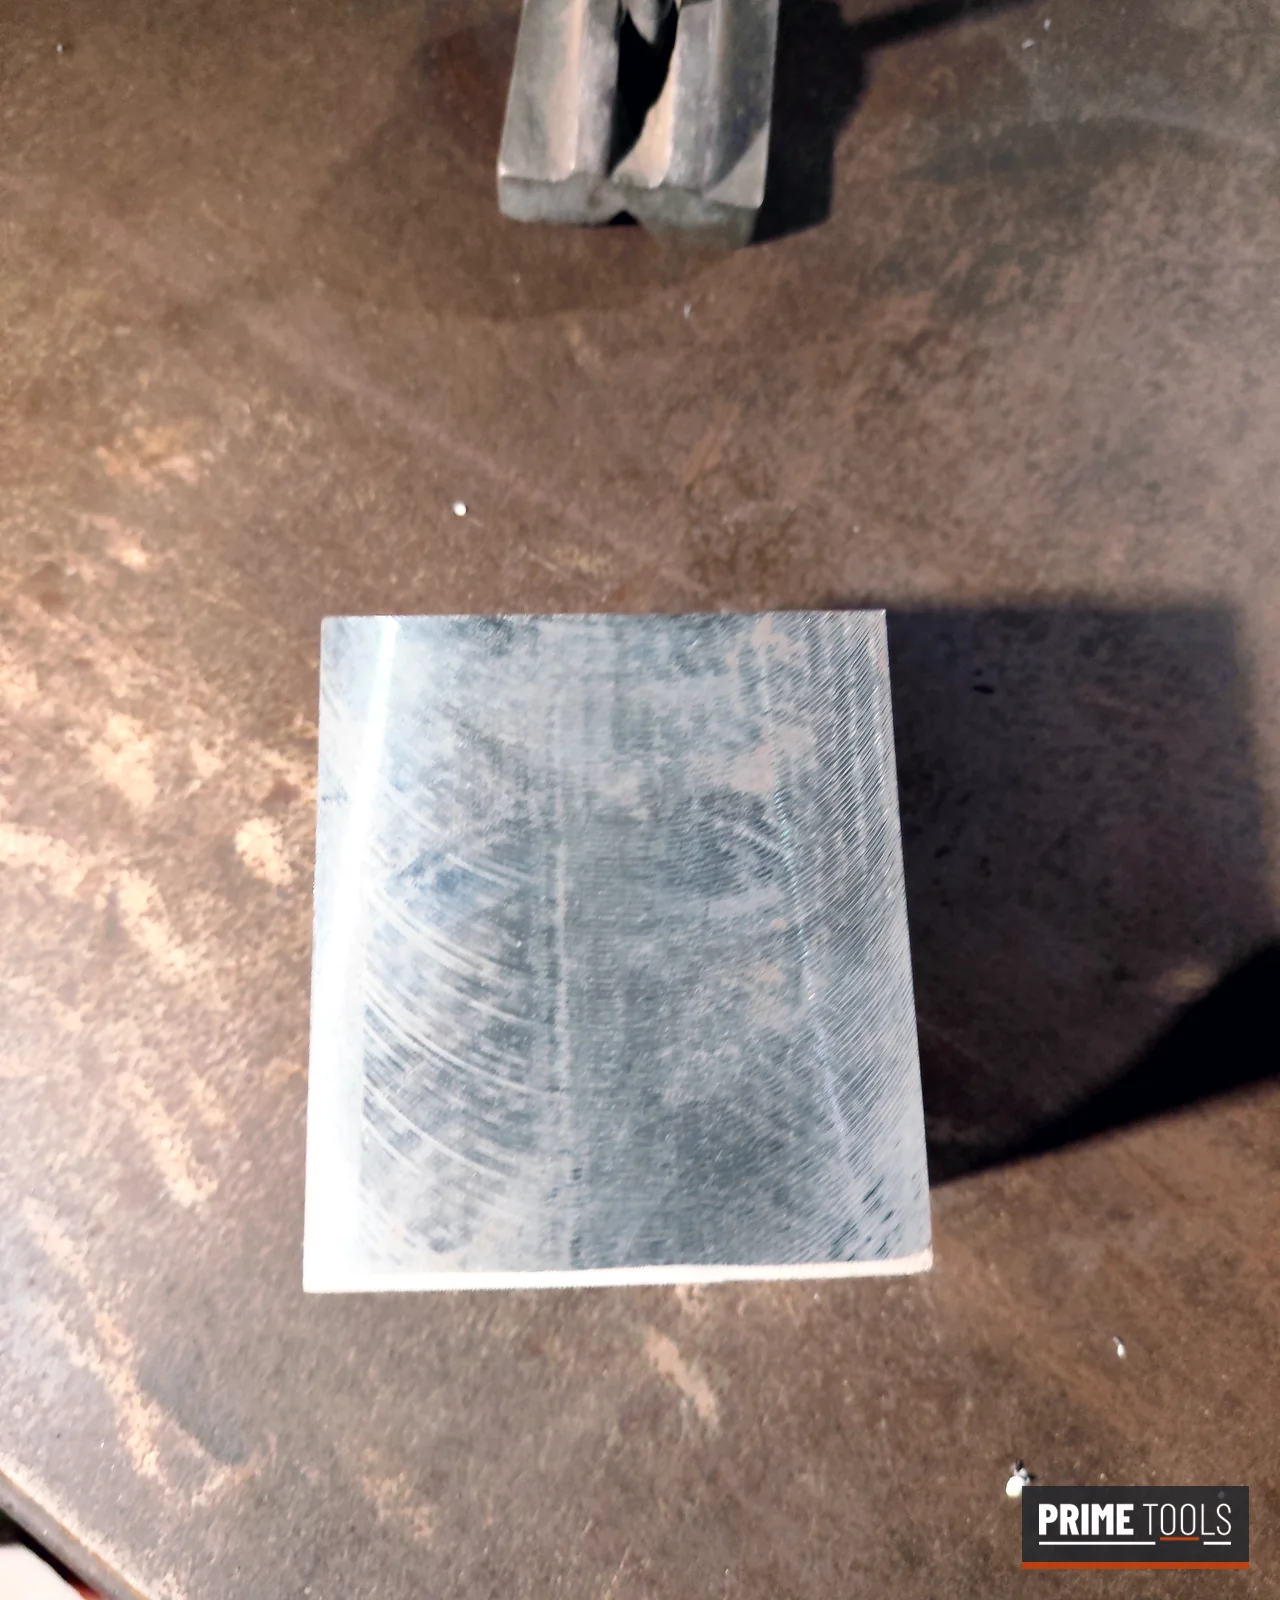
For the SMC lid from our 3D mould study, the cavity was machined from a solid block of Böhler W302 ESR, a hot-work steel that holds its polish and edges on long runs of abrasive compounds.
The block was squared, then roughed, semi-finished and finished on our BFW BMV 50 VMC with coolant, keeping enough stock for polishing and fitting. Machining in-house lets us control every stage and check sizes before the steel leaves the machine.
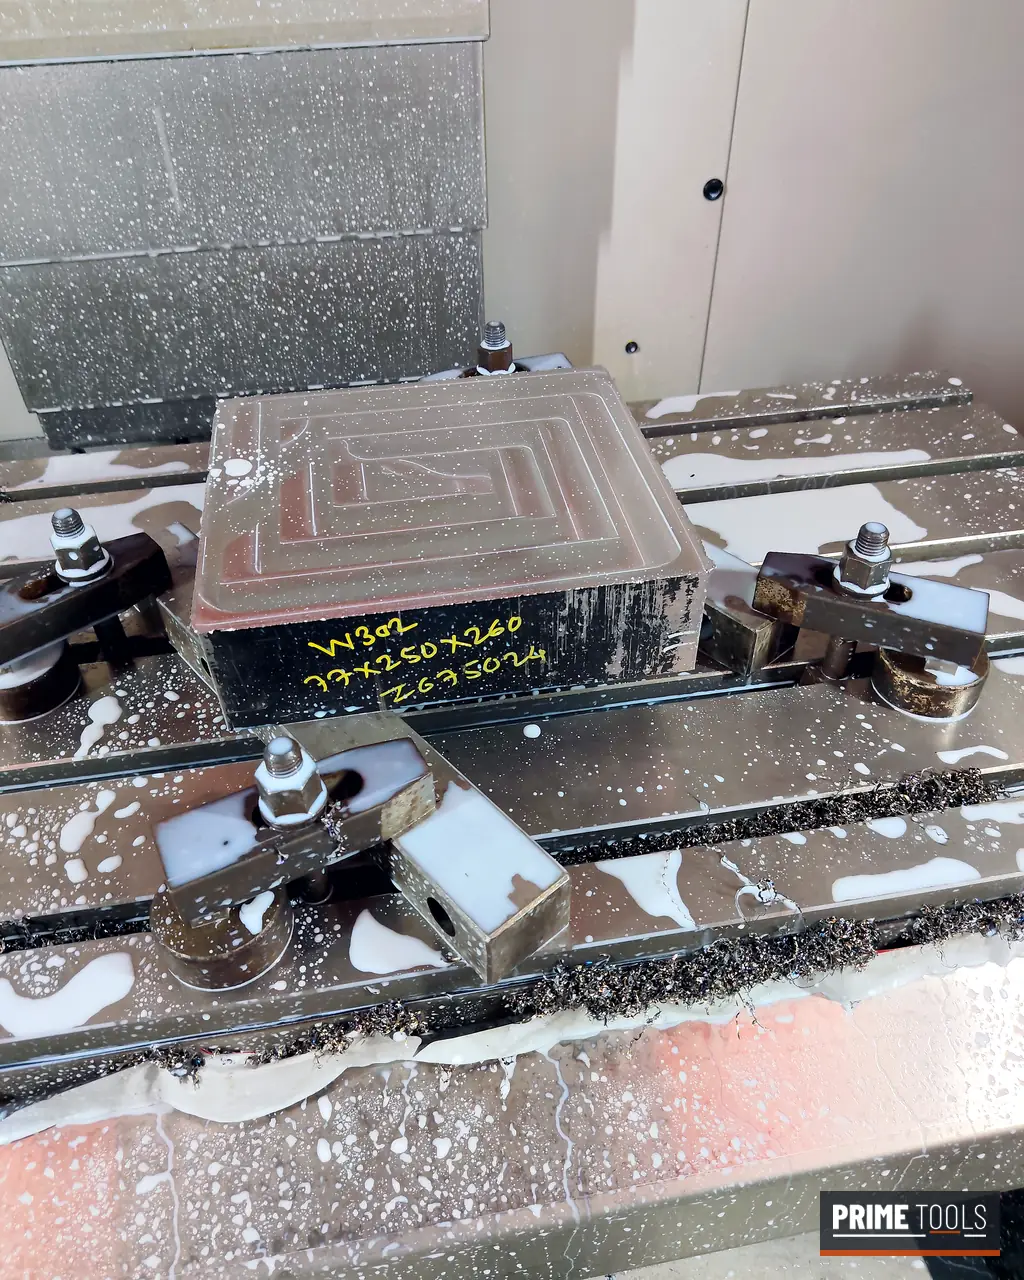
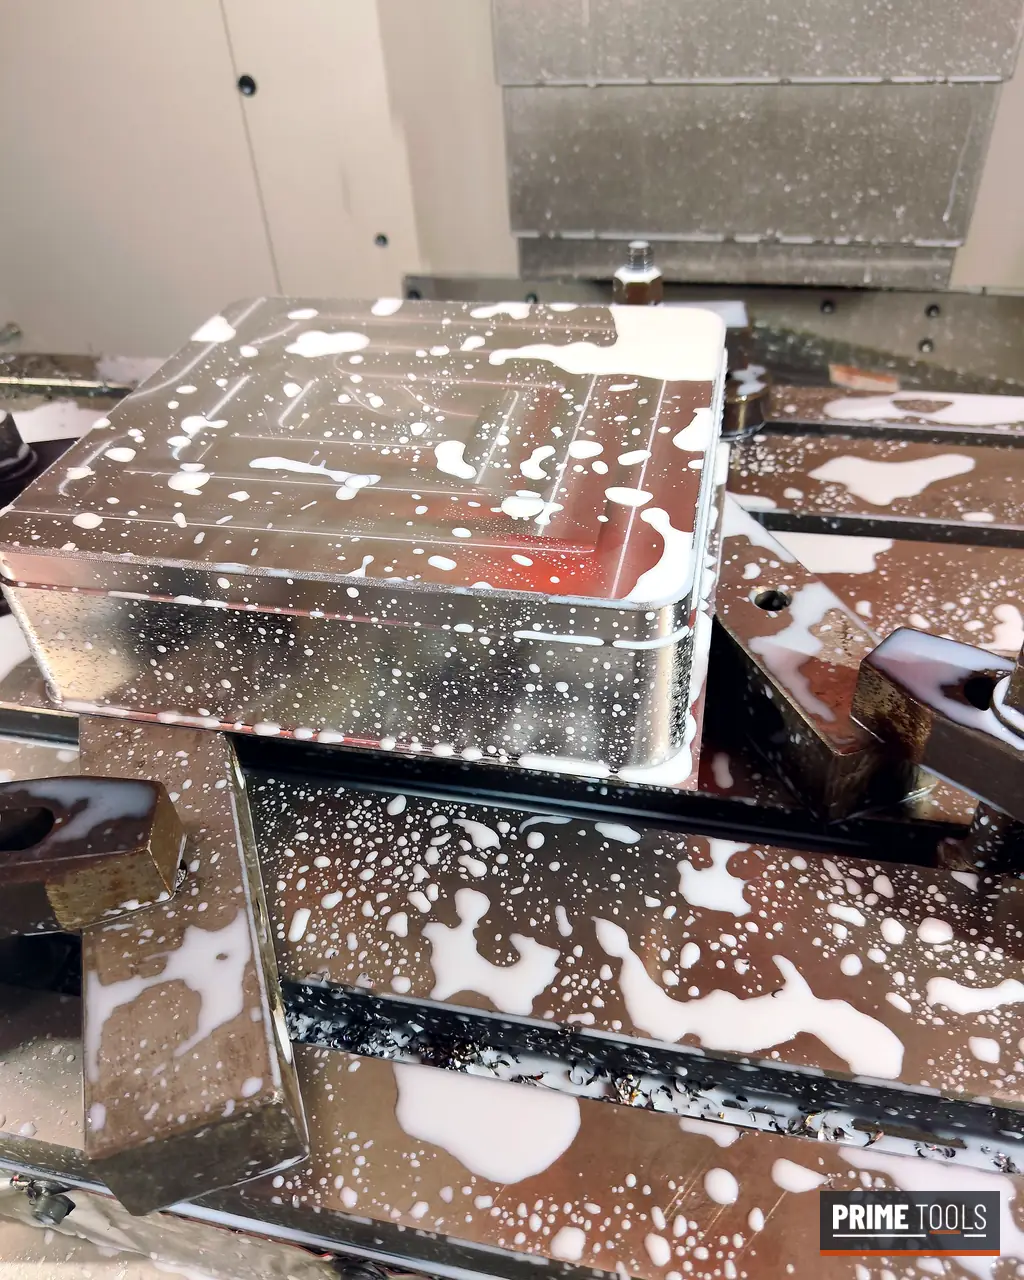
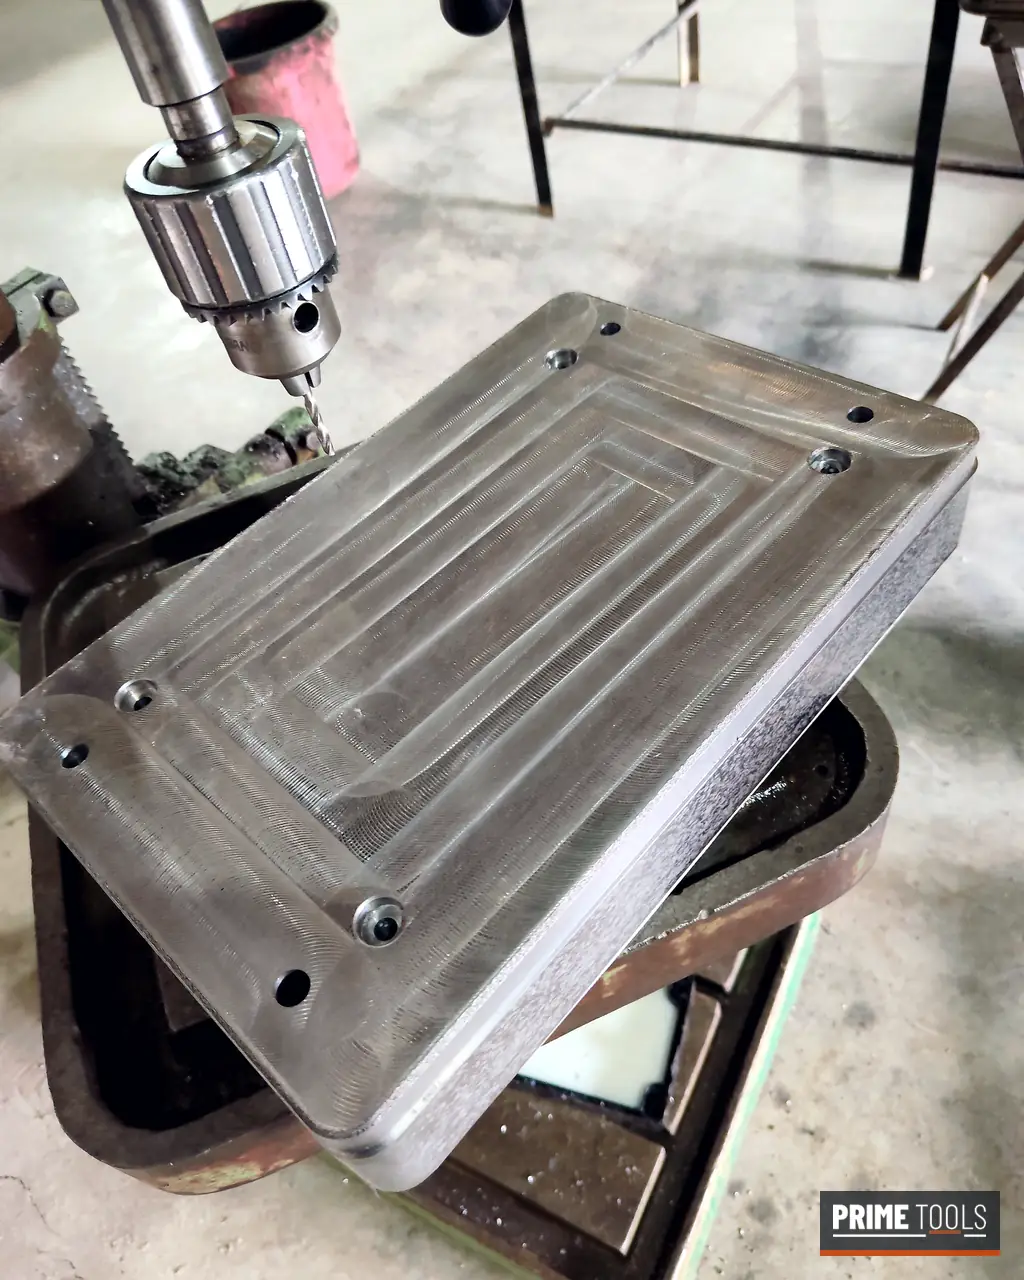
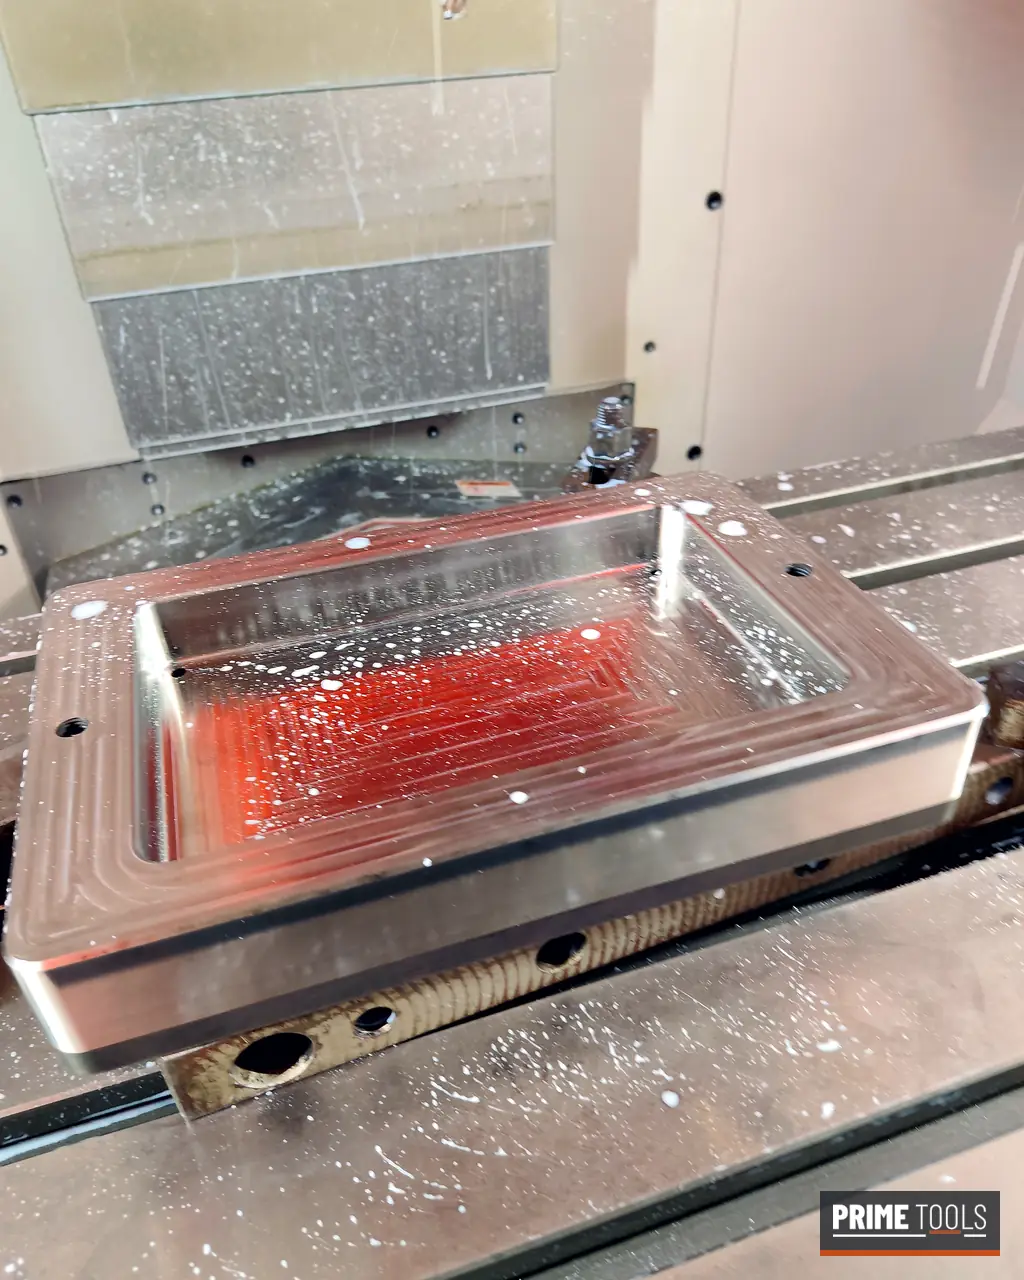
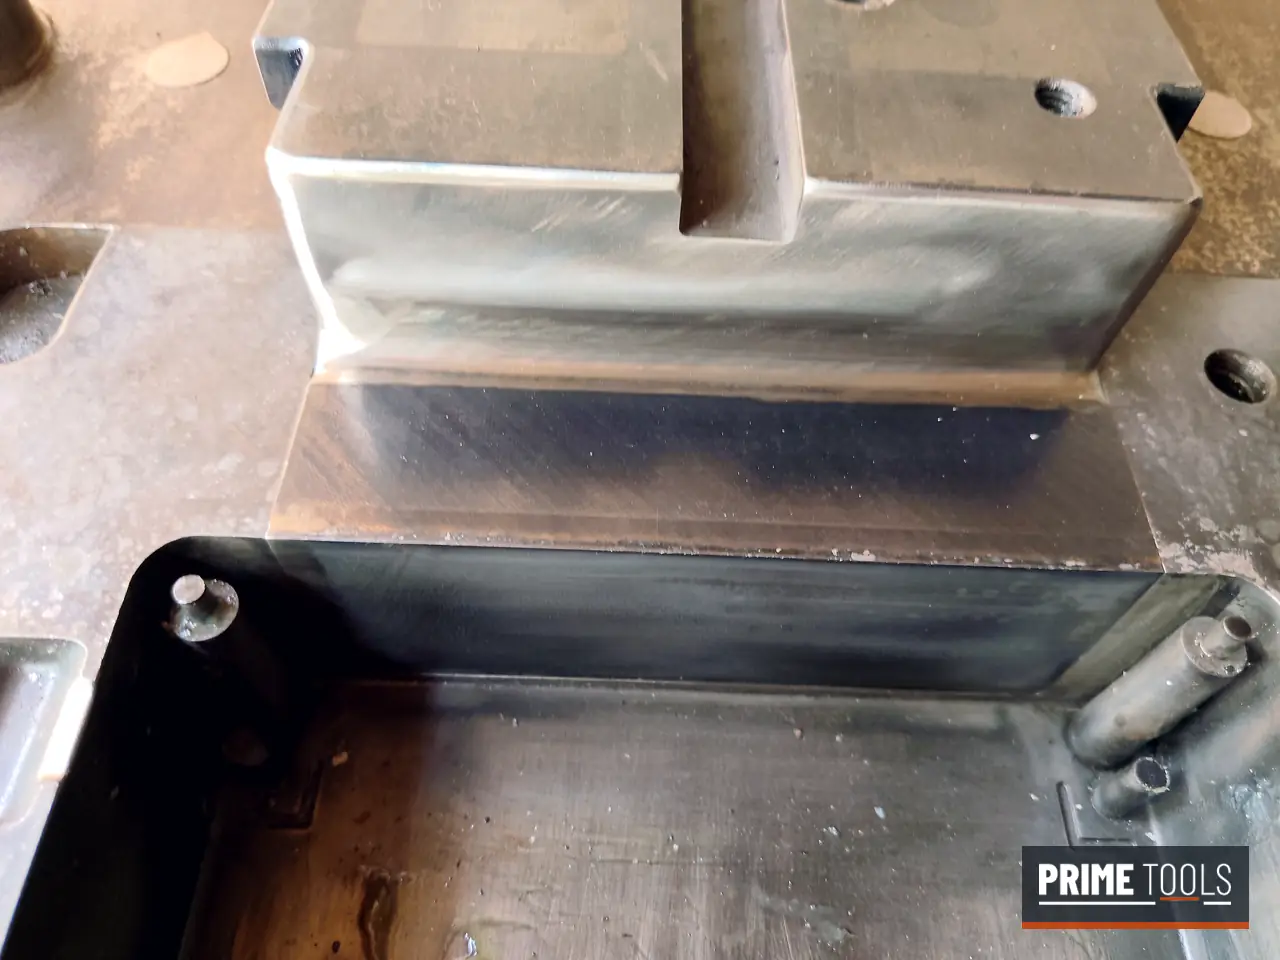
New lid cavity plate and core fit-up
A second lid cavity, machined on the VMC and then fitted to its core. Fitting is where a mould is won or lost: the shear edge must close evenly all the way round or the part flashes on one side and short-fills on the other.
Repair and die casting projects
Our repair, flash correction and die casting jobs, with before-and-after photos, are on their own pages: recent mould repair jobs and recent die casting jobs.
New HPDC inserts: from steel block to first castings
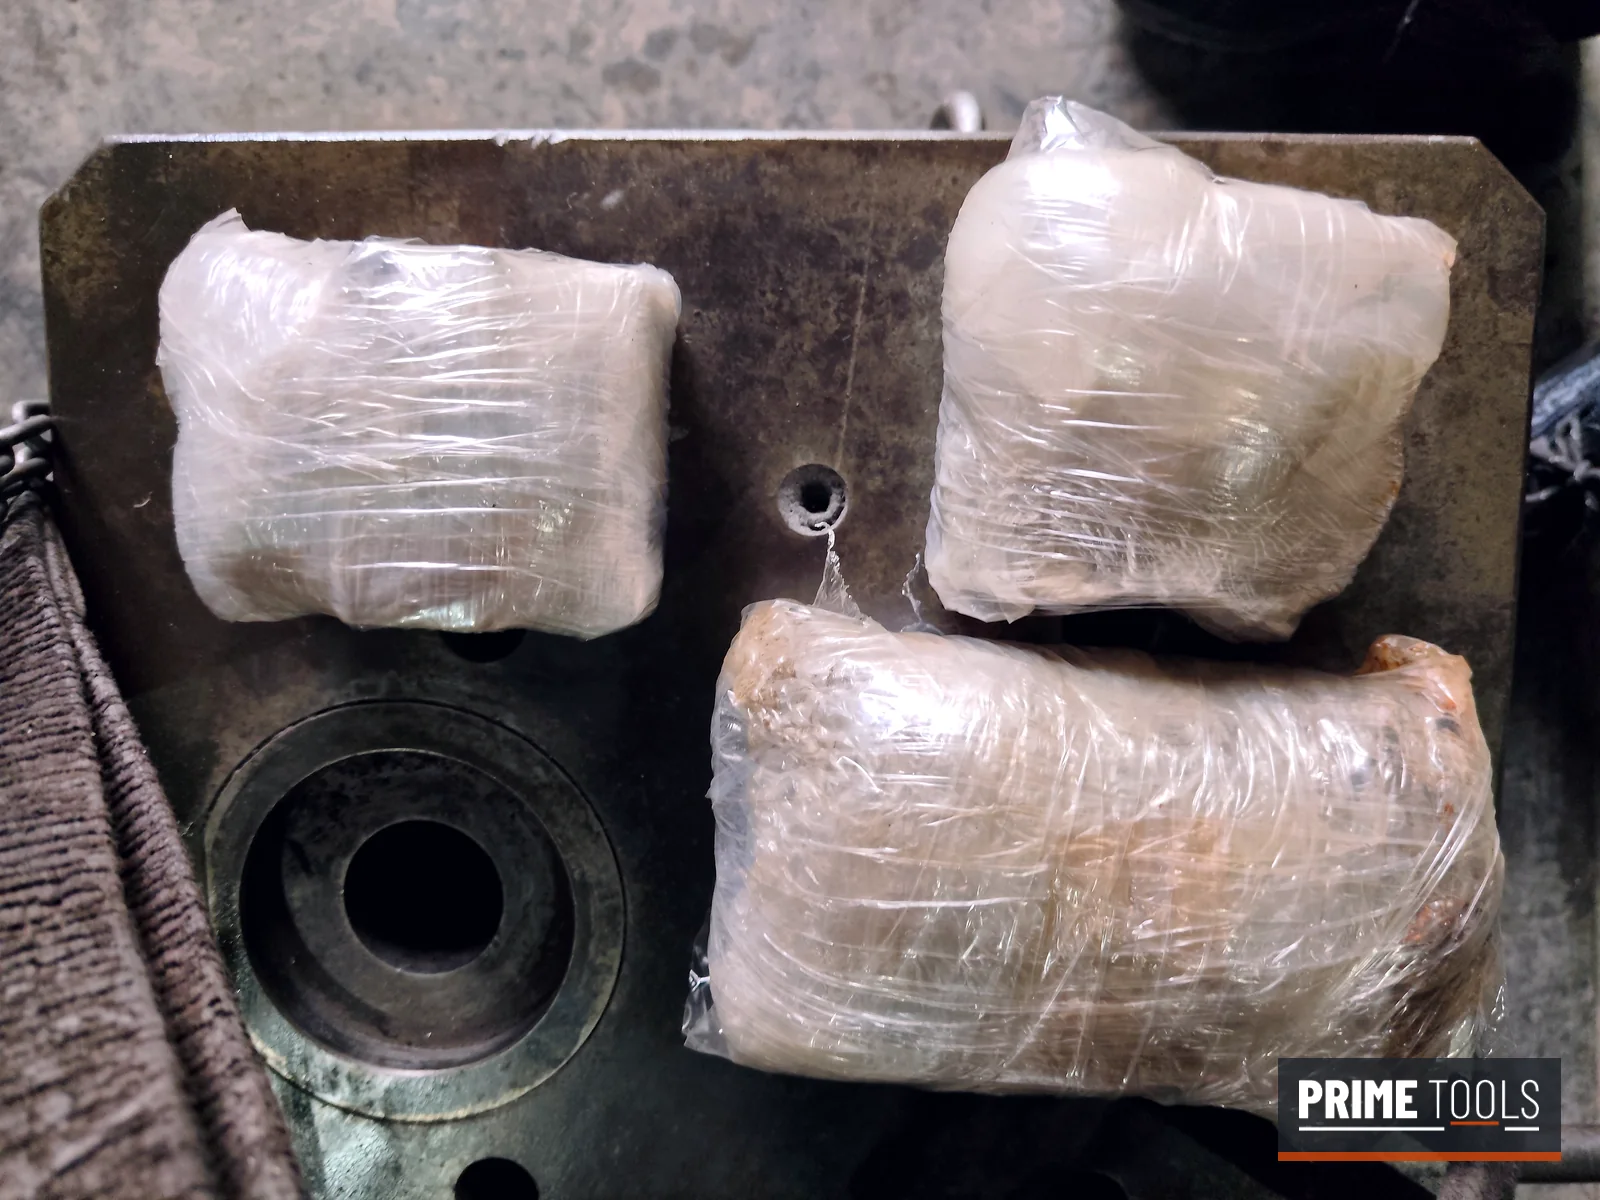
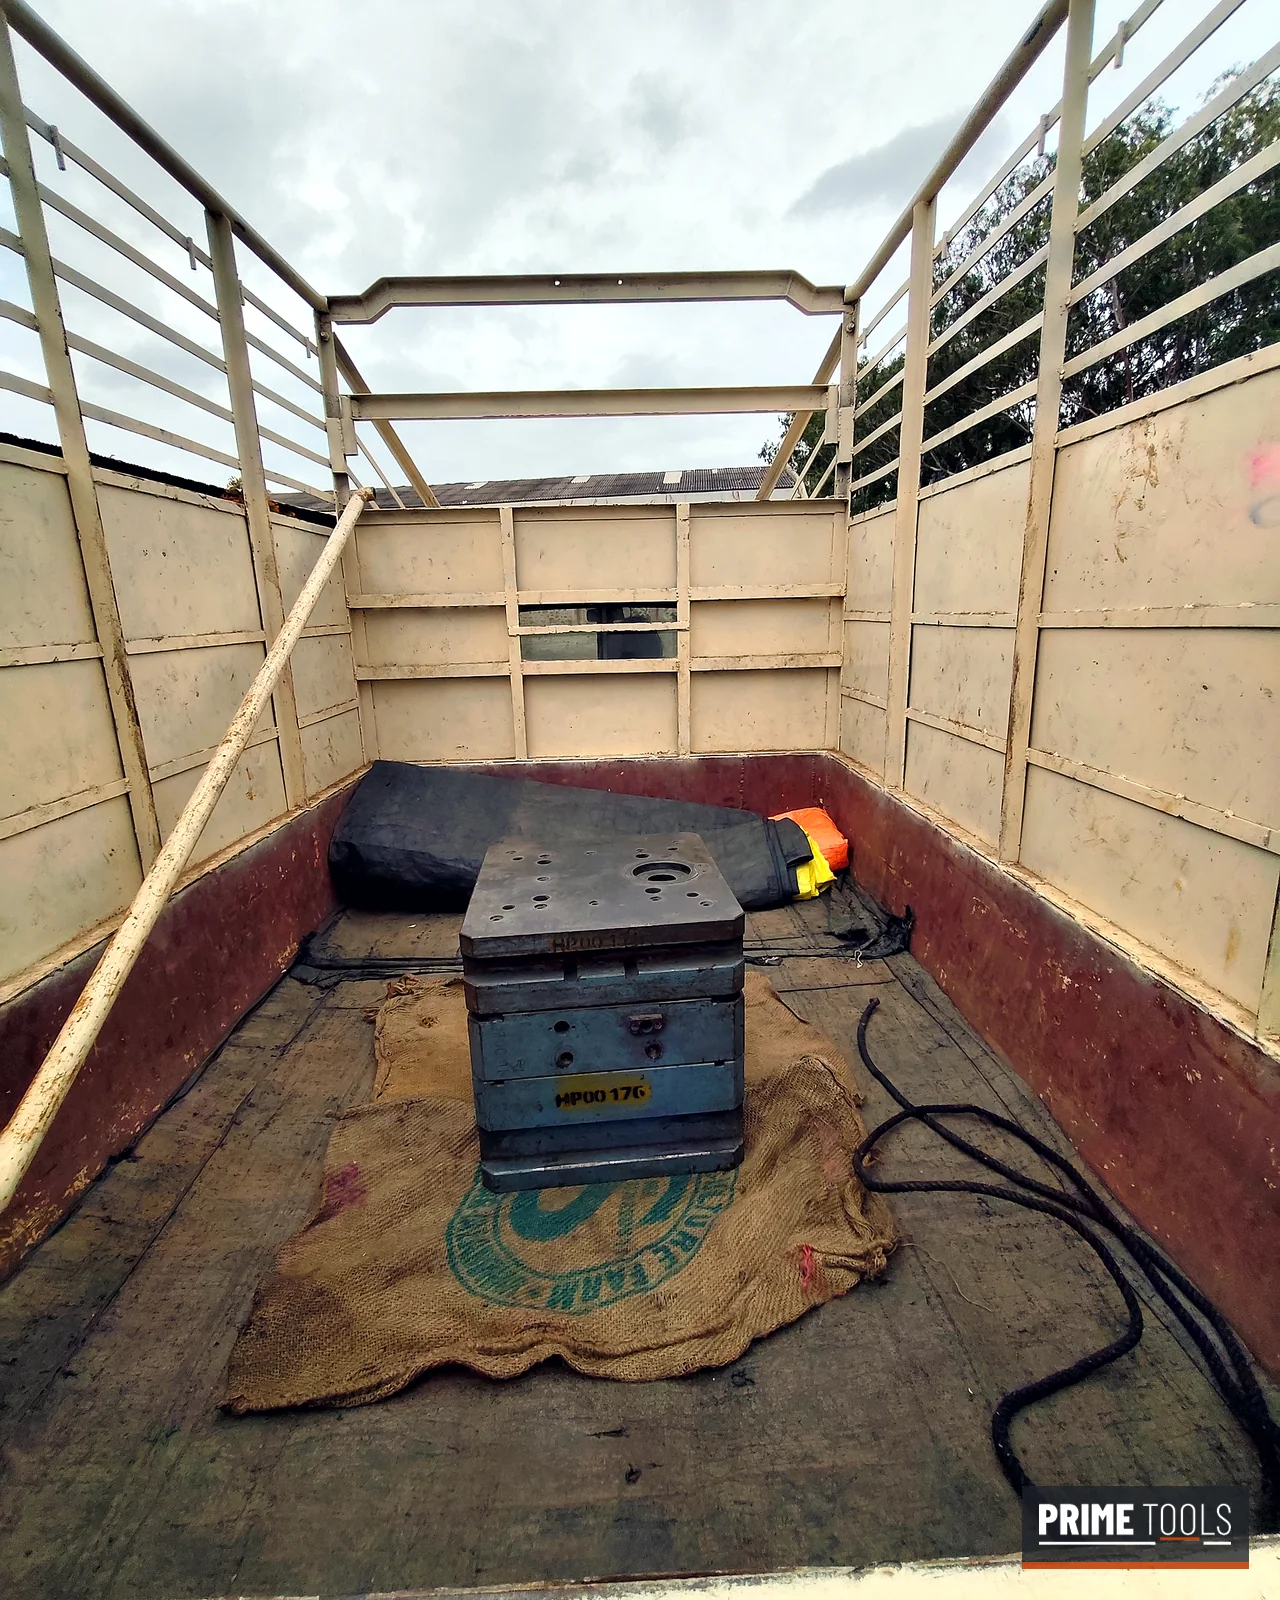
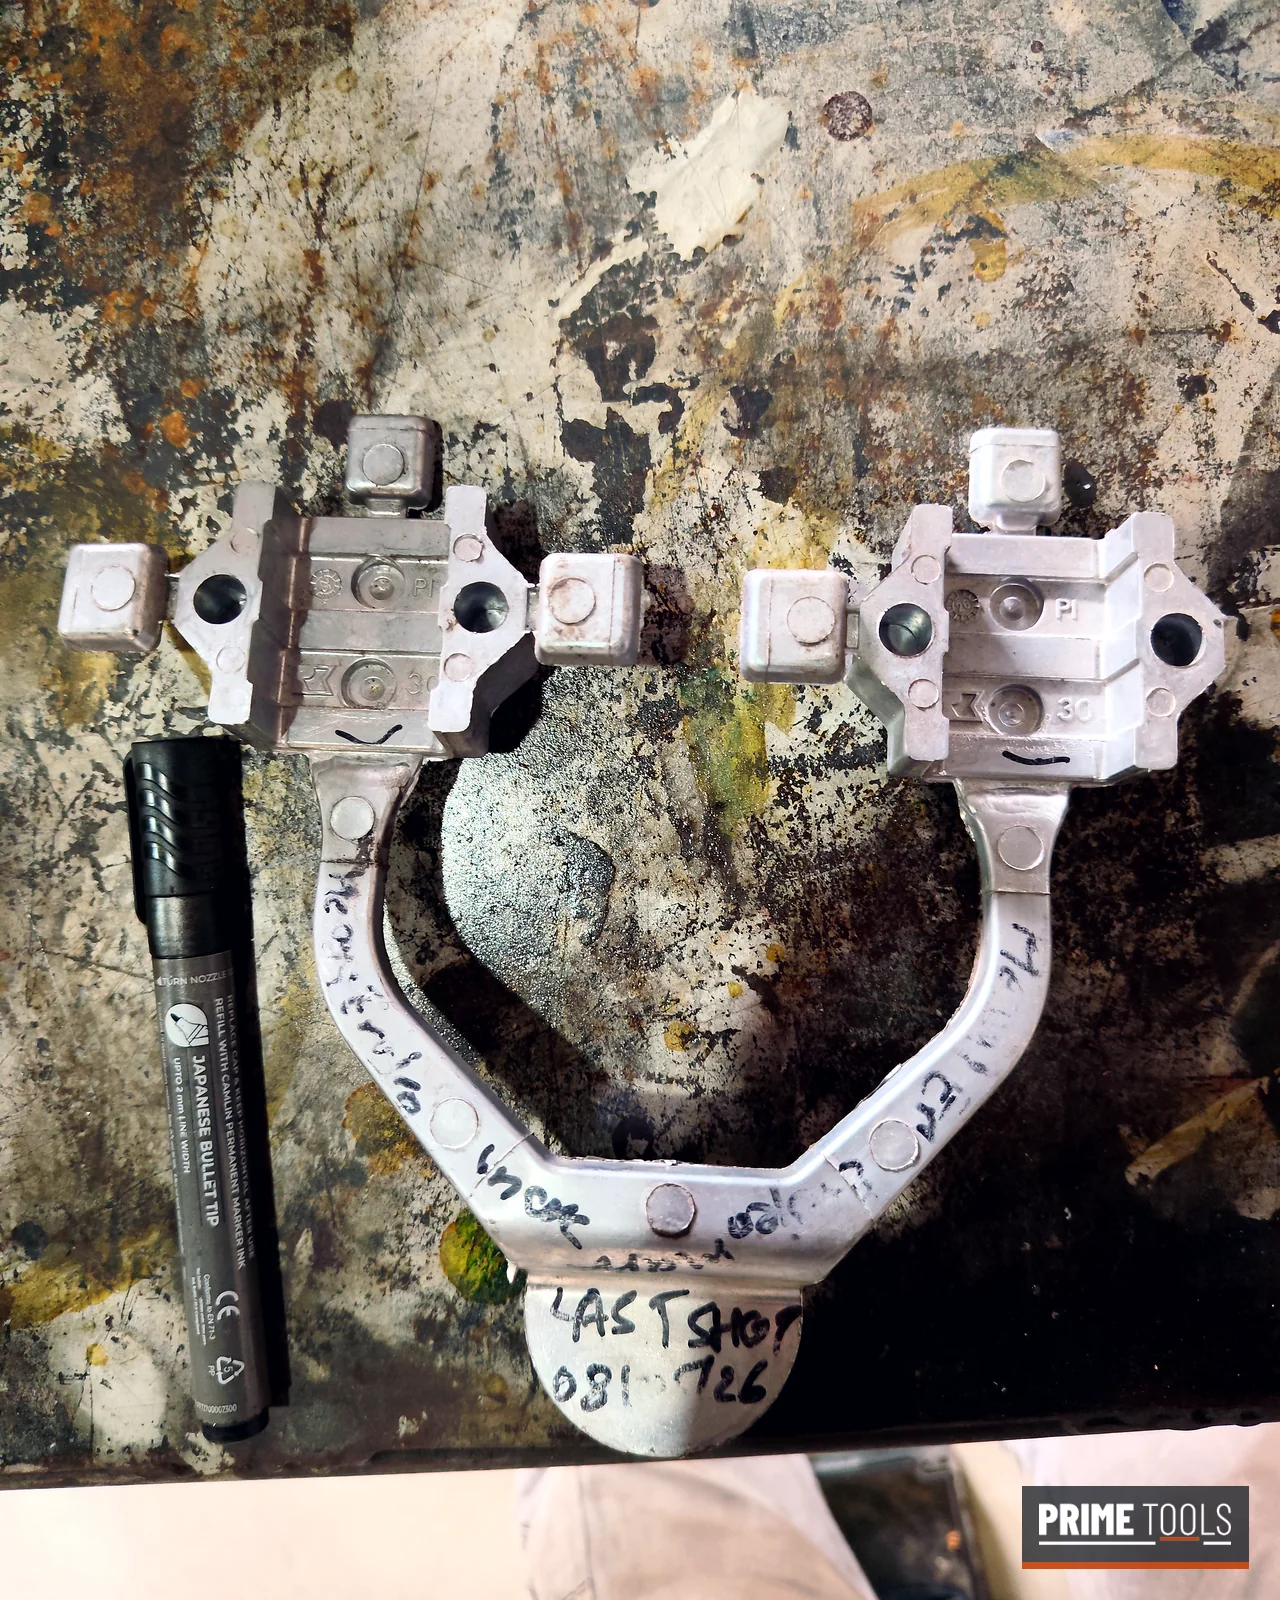
New core and cavity inserts for a high pressure die casting die: machined from tool steel in our tool room, fitted into the customer’s die and sent back for casting. The photos below follow the job from the steel block to the first castings made with the new inserts.
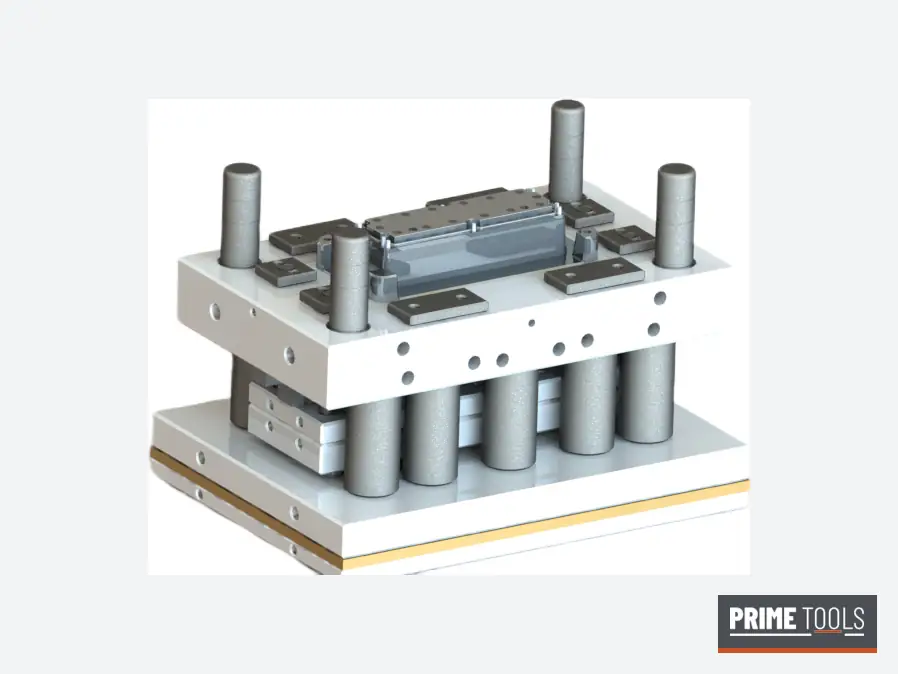
Mould design in 3D
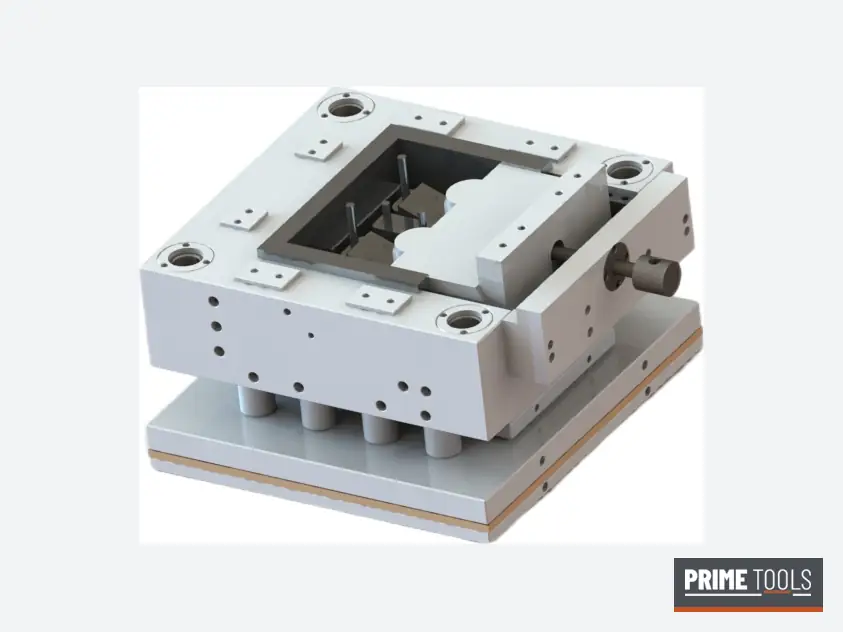
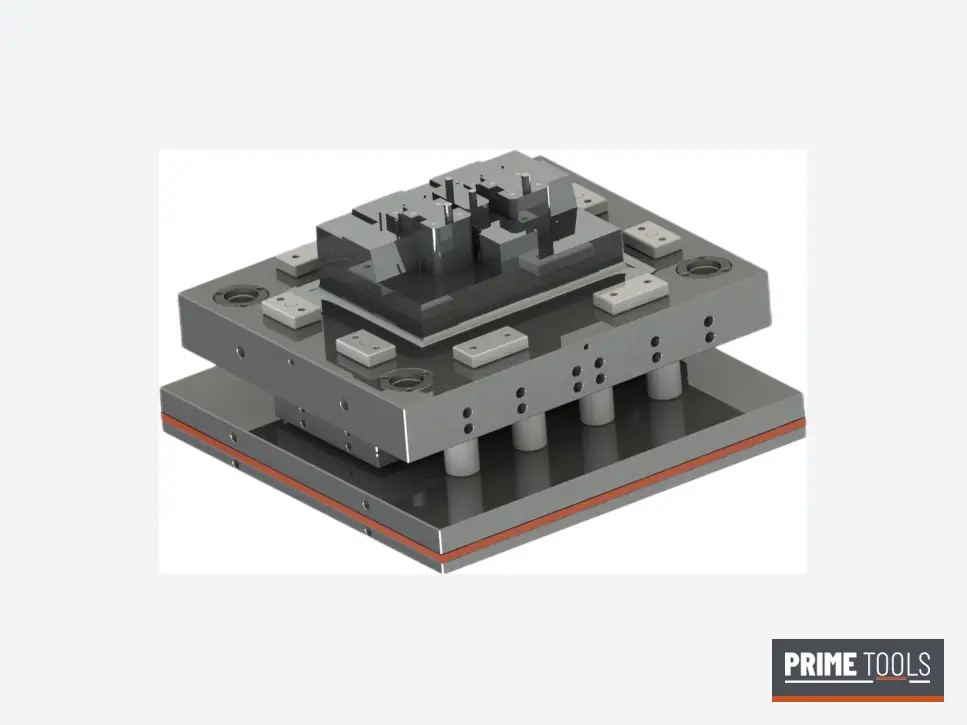
Every new mould is designed in 3D before any steel is ordered: plates, pillars, heating and ejection, with the part checked for draft and wall section in our DFM review.
Send your part for a free DFM review
3D model or drawing, material and annual volume. We reply within one working day.